Silo bulk material pneumatic conveying machines are essential equipment in industrial processes, designed to transport bulk materials such as powders, granules, and other particulate substances from one location to another within a silo or between silos. These systems leverage the principles of pneumatic transport to achieve efficient, dust-free, and continuous material handling, making them a preferred choice in various industrial applications.

Principle of Pneumatic Conveying for Silo Materials
The core principle of silo bulk material pneumatic conveying machines revolves around the use of compressed air or gas to create a flow that moves material through a pipeline. The system typically includes a hopper or silo for material storage, a conveying line, and a receiver or discharge point. As compressed air is introduced into the system, it creates a negative pressure or positive pressure environment that draws or pushes material through the pipeline. The design of the conveying line, including the diameter, length, and bends, is critical to ensure efficient material transport with minimal pressure loss and material degradation. The machine's control system manages the air flow and material feed, maintaining optimal operating conditions to prevent blockages and ensure consistent performance.

Working Scene Characteristics of Silo Pneumatic Conveying Machines
The working scene characteristics of silo bulk material pneumatic conveying machines are tailored to specific industrial environments, ensuring adaptability and efficiency. These systems are commonly used in industries such as food processing, pharmaceuticals, chemicals, and mining, where handling bulk materials requires precision and hygiene. The characteristics include:

- Space Efficiency: Pneumatic conveying systems are compact and can be installed in confined spaces, making them suitable for facilities with limited floor area. The vertical or horizontal configurations allow for flexible layout designs, optimizing space utilization.
- Dust Control: Unlike mechanical conveyors, pneumatic systems operate in a closed environment, significantly reducing dust emissions and improving workplace safety. This is particularly important in industries where dust can be hazardous or where product purity is critical.
- Material Handling Flexibility: These machines can handle a wide range of materials, from fine powders to coarse granules, with minimal adjustments. The ability to transport materials over long distances without the need for intermediate storage points enhances operational efficiency.
- Low Maintenance: Pneumatic conveying systems have fewer moving parts compared to mechanical alternatives, reducing the risk of wear and tear and lowering maintenance costs. The simplicity of the design contributes to longer service life and reduced downtime.
Application Scenarios and Operational Advantages
Silo bulk material pneumatic conveying machines are deployed in diverse operational scenarios, each leveraging the system's unique advantages. For example, in food processing plants, these machines are used to transport ingredients like flour, sugar, and spices from storage silos to production lines, ensuring a clean and efficient supply chain. In pharmaceutical facilities, the dust-free operation and hygienic design of the system meet stringent regulatory requirements, maintaining product integrity and safety. In chemical manufacturing, the ability to handle corrosive or abrasive materials without damage to the equipment is a key advantage, as the system's components are designed to withstand harsh conditions.
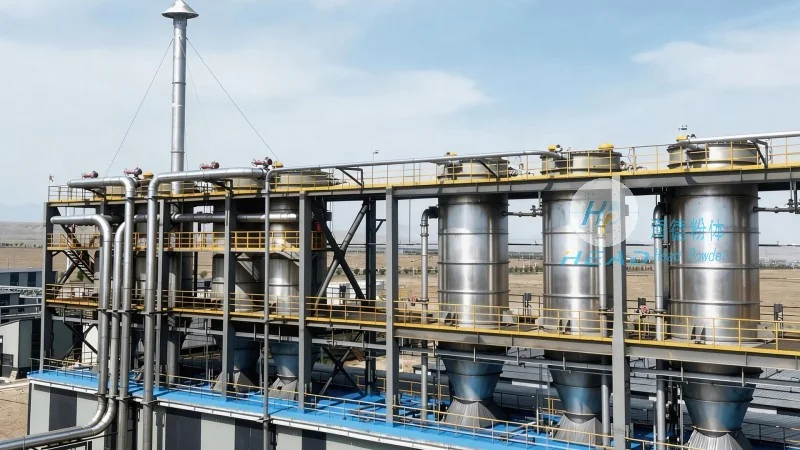
About HeadPowder: A Leading Provider of Pneumatic Conveying Solutions
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of silo bulk material pneumatic conveying machines. With headquarters in Shandong, China, HeadPowder specializes in developing customized solutions tailored to the specific needs of industrial clients. The company's commitment to quality and innovation has established it as a trusted partner in the industry, providing reliable equipment that meets international standards. HeadPowder's products are designed with durability, efficiency, and user safety in mind, ensuring long-term performance and customer satisfaction.




