HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment for stone aggregate powders. This article explores the working principle and key features of such systems, providing insights into their operational efficiency and practical applications.

Working Principle of Stone Aggregate Powder Pneumatic Conveying Equipment
The core of a stone aggregate powder pneumatic conveying system lies in its ability to transport bulk materials through an air stream. The process typically involves a few critical components: a material hopper, a conveying line, a blower or compressor, and a discharge outlet. When the system is activated, the blower generates high-pressure air that draws the stone aggregate powder from the hopper into the conveying line. The air stream, often referred to as the "carrier gas," moves the powder particles along the pipeline, ensuring a continuous and efficient flow. This method eliminates the need for mechanical components like belts or buckets, reducing wear and maintenance costs. The system can operate in both positive and negative pressure modes, allowing flexibility in material handling based on the application requirements.
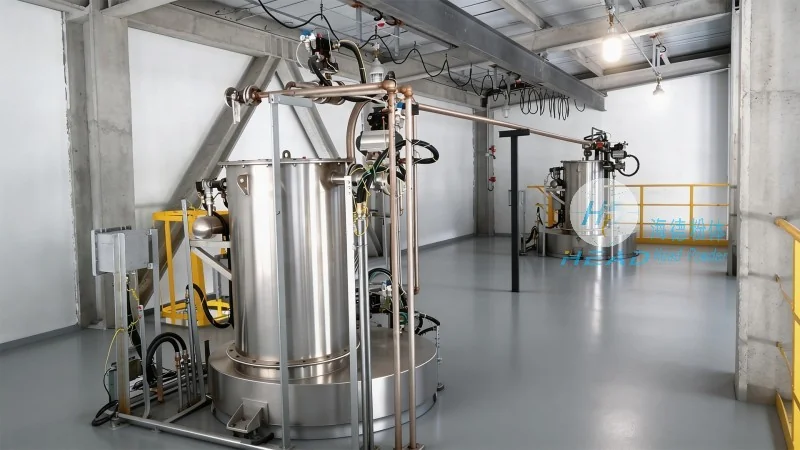
Key Features of Stone Aggregate Powder Pneumatic Conveying Equipment
Stone aggregate powder pneumatic conveying equipment from HeadPowder is engineered with several notable features that enhance performance and reliability. Firstly, the system offers high conveying efficiency, capable of transporting large volumes of powder over significant distances with minimal loss. This is achieved through optimized air flow and pipeline design, which minimizes particle segregation and ensures consistent material quality. Secondly, the equipment is designed for low maintenance, as the absence of moving parts reduces the risk of mechanical failure. This not only lowers operational costs but also increases the system's lifespan. Thirdly, the system is highly adaptable, with options for different pressure levels and material types, making it suitable for various industrial applications, from construction to mining. Additionally, the equipment is built with durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the abrasive nature of stone aggregate powders and ensure long-term durability. Environmental considerations are also addressed, as the system operates with minimal dust emissions, contributing to a cleaner working environment. Finally, the control systems are user-friendly, allowing operators to monitor and adjust the conveying process easily, ensuring optimal performance and safety.
Applications and Benefits in Industrial Settings
The working principle and features of stone aggregate powder pneumatic conveying equipment make it an ideal solution for industries dealing with bulk stone aggregate powders. In construction, these systems are used to transport sand, gravel, and other aggregates from storage to processing plants, improving workflow and reducing labor costs. In mining operations, the equipment efficiently moves crushed stone and other materials from processing areas to storage or transportation points. The benefits extend beyond efficiency, as the system enhances safety by eliminating the need for manual handling of heavy or dusty materials, reducing the risk of workplace injuries. Furthermore, the low dust emission and enclosed system design contribute to better air quality, aligning with environmental regulations and promoting a healthier work environment. The adaptability of the equipment allows it to be integrated into existing production lines with minimal modifications, making it a cost-effective upgrade for many industrial facilities.

Conclusion and Company Overview
Stone aggregate powder pneumatic conveying equipment, as explained, operates on a principle of air-driven transport, offering significant advantages in efficiency, maintenance, and adaptability. HeadPowder, with its headquarters in Shandong, China, has established itself as a trusted provider of such equipment, leveraging advanced engineering and quality materials to meet the diverse needs of industrial clients. The company's commitment to innovation and customer satisfaction ensures that its products not only meet but exceed industry standards, providing reliable solutions for material handling challenges. By understanding the working principle and features of these systems, industries can make informed decisions to enhance their operational capabilities and achieve greater productivity.




