Working Principle and Features of Calcium Hydroxide Pneumatic Conveying System Equipment
Release time:2026-09-17 08:01:23
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
The calcium hydroxide pneumatic conveying system operates based on the principle of air flow to transport bulk materials. In this system, a blower or compressor generates a high-velocity air stream that creates a negative pressure zone in the conveying line. The bulk material, such as calcium hydroxide powder, is fed into the system via a hopper or feeder. The air stream then lifts and transports the material through the pipeline to the destination point. The system typically includes components like a dust collector, filter, and control valve to ensure efficient and clean operation. The air is then filtered and recycled, minimizing waste and energy consumption.
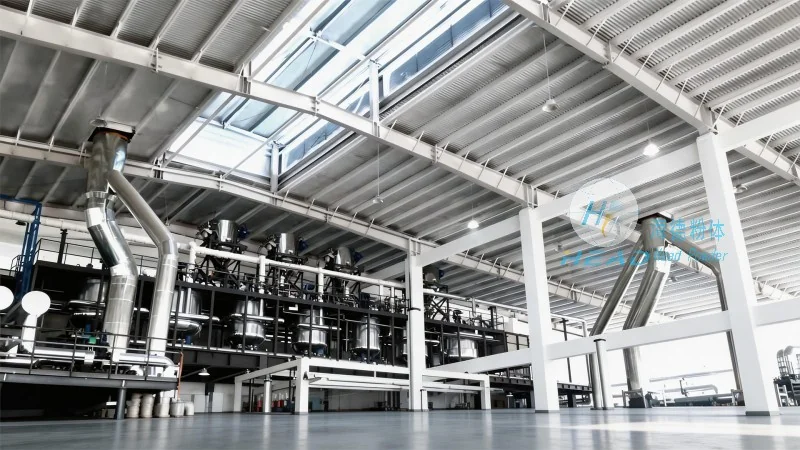

Key Features of Calcium Hydroxide Pneumatic Conveying Equipment
This equipment offers several key features that enhance its performance and usability. Firstly, it provides a dust-free and clean conveying process, which is crucial for handling calcium hydroxide, a material that can generate fine particles. The system is designed to maintain low pressure and high efficiency, ensuring stable material flow without clogging. Another feature is the adjustable air flow control, allowing operators to optimize the conveying rate based on the material's characteristics and pipeline length. The equipment also includes safety features such as pressure relief valves and emergency shut-off mechanisms to prevent accidents. Additionally, the system is compact and easy to install, making it suitable for various industrial applications, including chemical processing, food production, and pharmaceutical manufacturing.
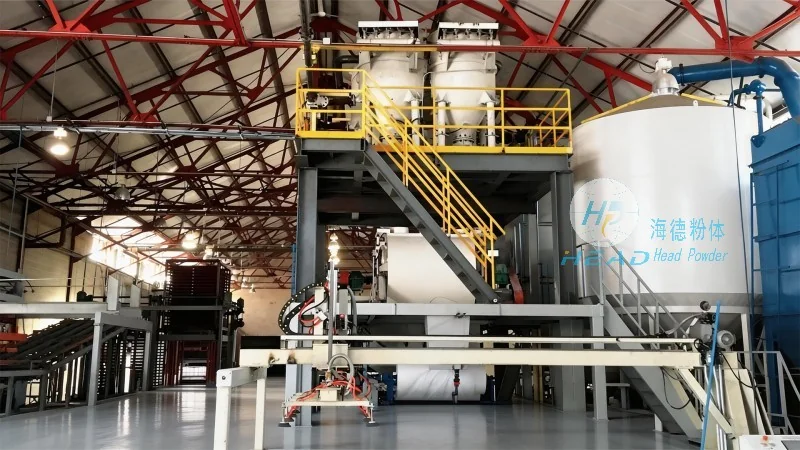
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in pneumatic conveying systems and related equipment. With a focus on innovation and quality, the company has developed advanced solutions for transporting bulk materials efficiently and safely. HeadPowder's products are designed to meet the specific needs of industries handling calcium hydroxide and other fine powders, ensuring reliable performance and minimal downtime. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the chemical and material handling sectors.

Advantages of Using Calcium Hydroxide Pneumatic Conveying Systems
Implementing a pneumatic conveying system for calcium hydroxide offers numerous advantages over traditional methods like belt conveyors or bucket elevators. The primary benefit is the ability to transport the material in a closed system, which prevents dust contamination and improves workplace safety. This is particularly important for calcium hydroxide, which can cause respiratory issues if inhaled. Additionally, the system reduces material loss and waste, as the conveying process is enclosed and the material is not exposed to the environment. From an operational perspective, the system offers higher efficiency and lower maintenance costs compared to other methods. The adjustable air flow allows for precise control over the conveying rate, ensuring that the material is delivered to the destination at the desired speed. Furthermore, the system is energy-efficient, as the air is recycled and reused, reducing energy consumption and operational costs.




