Dust-free closed-circuit pneumatic conveying systems represent a sophisticated method for transporting bulk materials in industrial settings. These systems are designed to handle a wide range of powders and granules while maintaining a completely sealed environment, preventing dust emissions and ensuring operational safety. The technology is widely adopted across various industries, including food processing, pharmaceuticals, chemicals, and minerals, where material integrity and environmental compliance are critical.
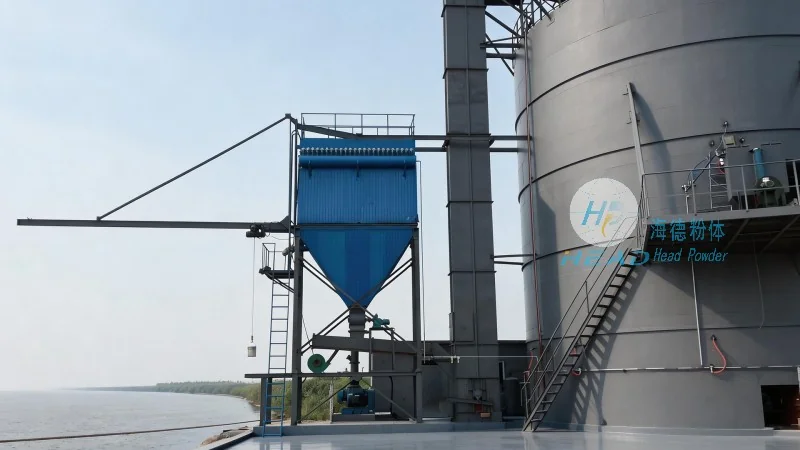
Structural Components and Working Principle
The core components of a dust-free closed-circuit pneumatic conveying system typically include a material feed hopper, a conveying pipeline, a separation unit (such as a cyclone or filter), and a return air system. The process begins with the material being fed into the hopper, where it is then drawn into the pipeline by a positive displacement blower or a rotary lobe pump. The air, carrying the material particles, travels through the pipeline to the separation unit. Here, the air and material are separated; the material is collected and returned to the system, while the air is filtered and recirculated back to the blower. This closed-loop design ensures that no material is lost to the environment and that the system operates efficiently with minimal air consumption.
Key Advantages of Dust-Free Pneumatic Conveying
One of the primary advantages of dust-free closed-circuit systems is their ability to maintain a clean and safe working environment. By containing all material handling within a sealed system, these systems eliminate dust emissions, reducing the risk of respiratory issues and contamination. Additionally, the closed-loop design minimizes material waste, as the system recovers and reuses the conveyed material, leading to cost savings and improved operational efficiency. The technology also offers flexibility in material handling, allowing for the transport of materials over long distances and varying elevations without the need for complex mechanical components.

Applications in Industrial Processes
Dust-free closed-circuit pneumatic conveying is utilized in numerous industrial applications where material handling demands precision and environmental control. In the food industry, for example, these systems are employed to transport ingredients like flour, sugar, and spices, ensuring that the products remain free from contamination and retain their quality. In the pharmaceutical sector, the sealed environment is crucial for maintaining the sterility of active ingredients and preventing cross-contamination. Similarly, in chemical and mineral processing, the technology helps in transporting powders and granules while adhering to strict safety and environmental regulations.

Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and installation of dust-free pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder's expertise lies in customizing conveying solutions to meet the specific needs of clients, ensuring that each system is optimized for efficiency, reliability, and environmental compliance. The company's facilities are located in Shandong, China, where it leverages advanced manufacturing capabilities and technical expertise to deliver high-performance conveying systems.

Technical Capabilities and Service
HeadPowder employs a team of experienced engineers and technicians who are well-versed in the principles of pneumatic conveying. The company offers comprehensive services, including system design, material testing, and on-site installation and commissioning. By working closely with clients, HeadPowder ensures that the conveying systems are tailored to the unique characteristics of the materials being handled, such as particle size, density, and moisture content. This personalized approach helps in maximizing the system's performance and longevity. Furthermore, the company provides ongoing support and maintenance services to ensure that the systems operate at peak efficiency throughout their service life.
Conclusion
Dust-free closed-circuit pneumatic conveying systems represent a significant advancement in material handling technology, offering a safe, efficient, and environmentally friendly solution for transporting bulk materials. With the expertise and commitment of companies like Shandong HeadPowder Engineering Co., Ltd., these systems are becoming increasingly prevalent in industrial applications worldwide. As industries continue to prioritize safety and sustainability, the demand for advanced pneumatic conveying solutions is expected to grow, making it an essential technology for modern manufacturing processes.




