Ammonium bicarbonate is a widely used chemical in various industrial applications, and efficient powder conveying systems are crucial for its handling and transportation. This article explores the principles and operational characteristics of the ammonium bicarbonate powder conveying system equipment, focusing on its design, functionality, and typical application scenarios.

Overview of Ammonium Bicarbonate Powder Conveying Systems
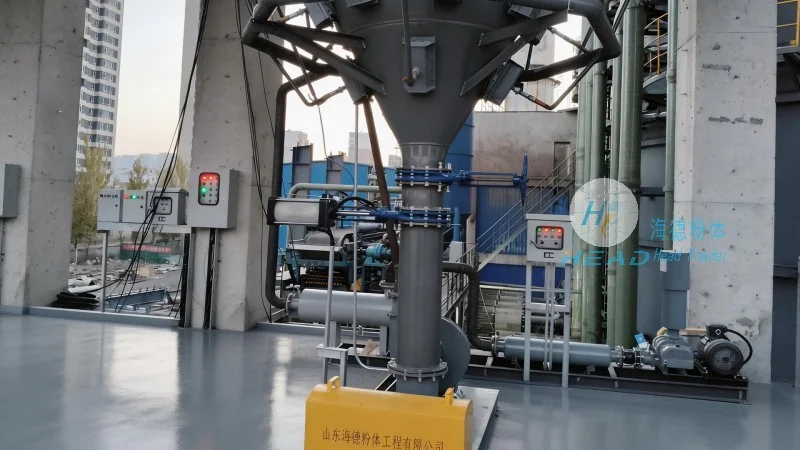
Ammonium bicarbonate powder conveying systems are engineered to handle the unique properties of ammonium bicarbonate, such as its hygroscopic nature and potential for caking. These systems are designed to ensure safe, reliable, and efficient transport of the material from storage to processing or packaging areas. The equipment typically includes components like hoppers, feeders, conveyors, and control systems, all tailored to maintain the material's quality and prevent degradation during handling.
The Core Principles of the Conveying System
The operation of ammonium bicarbonate powder conveying systems is based on several key principles. First, the system must address the material's tendency to absorb moisture from the air, which can lead to clumping and blockages. To mitigate this, the equipment often incorporates drying or moisture control mechanisms, such as heated hoppers or desiccant systems. Second, the design prioritizes minimizing friction and abrasion to prevent material degradation, as ammonium bicarbonate is sensitive to mechanical stress. Third, the system ensures uniform flow and consistent pressure to maintain stable conveying rates, which is critical for downstream processes.

Working Scene Characteristics and Application Scenarios
The working scene characteristics of ammonium bicarbonate powder conveying systems vary based on the specific industrial environment. In agricultural chemical production, for example, the system may be integrated into large-scale fertilizer manufacturing facilities, where the material is transported from bulk storage to mixing and granulation units. The system must handle high volumes of ammonium bicarbonate while maintaining low dust emissions and preventing contamination from other materials. In pharmaceutical or food processing applications, the conveying system is designed for more stringent hygiene standards, with enclosed and sealed components to avoid cross-contamination and ensure product purity.
Key Components and Their Functions
Several critical components make up the ammonium bicarbonate powder conveying system. The hopper serves as the storage vessel, often equipped with a discharge valve to control the flow of material. The feeder, typically a rotary or vibratory type, regulates the material feed rate to the conveyor, ensuring consistent and controlled transport. The conveyor itself, which may be a pneumatic or mechanical system, moves the powder through the system. Control systems, including sensors and automation, monitor parameters like pressure, flow rate, and temperature to maintain optimal operation and detect any anomalies.

Advantages and Benefits in Practical Applications
Implementing an ammonium bicarbonate powder conveying system offers several advantages. The system enhances operational efficiency by reducing downtime caused by blockages or material degradation. It improves safety by minimizing dust exposure and preventing accidental spills. Additionally, the controlled conveying process ensures that the material reaches its destination in the correct condition, maintaining product quality and reducing waste. For companies like Shandong HeadPowder Engineering Co., Ltd., based in China, these systems are designed to meet the specific needs of their clients, providing customized solutions that enhance productivity and reliability.




