High-alumina fly ash powder pneumatic conveying systems represent a critical technology in modern industrial material handling, particularly for the efficient and safe transport of high-alumina fly ash—a byproduct commonly found in power generation facilities. The system's design and operation are tailored to meet the demanding requirements of handling such powders, ensuring minimal dust generation, high conveying efficiency, and reliable performance under various operational conditions.

Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner for industries requiring sophisticated material handling solutions. HeadPowder's expertise lies in developing customized systems that address the unique challenges of transporting high-alumina fly ash, a material known for its abrasive and fine particle characteristics.
System Overview and Key Components
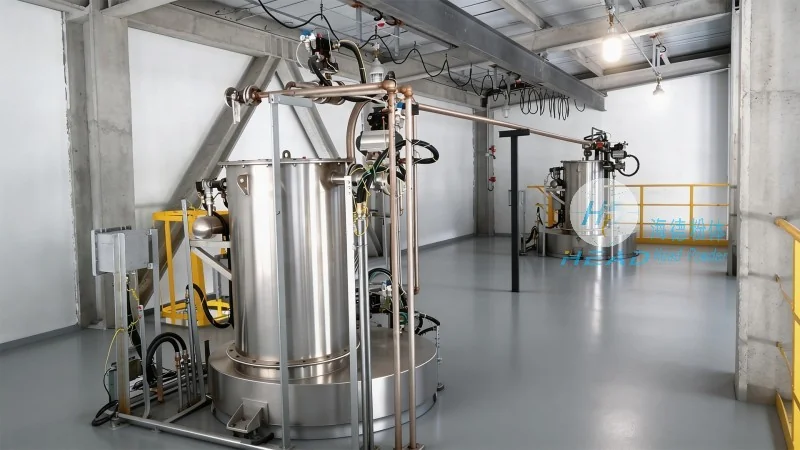
The high-alumina fly ash powder pneumatic conveying system typically consists of several core components that work in tandem to achieve efficient material transport. These components include a hopper for material storage, a rotary airlock valve for controlled discharge, a positive displacement blower or air compressor to generate the necessary air pressure, a pipeline network for conveying the material, and a receiver or collection unit at the destination. Each component plays a crucial role in ensuring the system operates smoothly and reliably.
Operation Process: Step-by-Step Execution
The operation of the high-alumina fly ash powder pneumatic conveying system follows a systematic process, starting with material loading into the hopper. The rotary airlock valve regulates the flow of fly ash from the hopper into the conveying line, preventing backflow and maintaining consistent material feed. Simultaneously, the blower generates a high-pressure air stream that propels the fly ash particles through the pipeline. As the material travels, it is suspended and transported by the air flow, with the pipeline design optimized to minimize pressure drop and ensure efficient transport. At the receiving end, the material is deposited into the collection unit, and the air is filtered and returned to the system or released safely.

Working Principle: The Physics Behind Pneumatic Conveying
The working principle of the high-alumina fly ash powder pneumatic conveying system is based on the fundamental physics of fluid dynamics and particle suspension. When air is forced through the pipeline at a sufficient velocity, it creates a pressure differential that lifts and transports the fly ash particles. The key to successful conveying lies in achieving the correct air velocity and pressure to maintain particle suspension without causing excessive wear on the system components. The system's design considers factors such as particle size, density, and moisture content of the fly ash to optimize conveying parameters. By carefully balancing these variables, the system ensures high conveying efficiency and minimal energy consumption.
Advantages and Technical Benefits
High-alumina fly ash powder pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These include reduced dust generation, which enhances workplace safety and compliance with environmental regulations. The system also provides a more hygienic and controlled environment for handling fine powders, minimizing the risk of contamination. Additionally, pneumatic conveying systems can handle abrasive materials like high-alumina fly ash without significant wear on components, thanks to the protective effect of the air flow. The compact design of the system allows for easy integration into existing industrial facilities, and the modular construction enables flexible customization to meet specific application requirements.
Applications and Industry Impact
High-alumina fly ash powder pneumatic conveying systems are widely used in various industries, including power generation, cement production, and industrial waste management. In power plants, the system efficiently transports fly ash from boiler ash hoppers to storage or disposal facilities, improving operational efficiency and reducing manual handling risks. In cement plants, the system aids in the transport of fly ash as a supplementary cementitious material, contributing to the production of high-quality concrete. The technology's adaptability makes it suitable for a range of applications where the safe and efficient handling of fine powders is critical.
Maintenance and Operational Considerations
To ensure the long-term reliability and performance of the high-alumina fly ash powder pneumatic conveying system, regular maintenance is essential. This includes monitoring air pressure and flow rates, inspecting components for wear and tear, and cleaning the system to prevent clogging. The system's design incorporates features such as wear-resistant liners and robust blower components to extend the lifespan of critical parts. Additionally, proper training of operators and adherence to safety protocols are crucial for maintaining optimal system performance and preventing accidents. By following recommended maintenance schedules and operational guidelines, users can maximize the system's efficiency and minimize downtime.
Conclusion: The Role of Advanced Pneumatic Conveying
High-alumina fly ash powder pneumatic conveying systems represent a sophisticated solution for the efficient and safe handling of fine industrial powders. Developed by companies like Shandong HeadPowder Engineering Co., Ltd., these systems combine advanced engineering principles with practical application to address the unique challenges of transporting high-alumina fly ash. By understanding the operation process and working principles of such systems, industries can enhance their material handling capabilities, improve operational efficiency, and ensure compliance with safety and environmental standards. The continued development and refinement of pneumatic conveying technology will likely play an increasingly important role in the future of industrial material handling, particularly as industries strive for more sustainable and efficient processes.




