For industrial operations that require efficient, clean, and safe handling of bulk powders, the dust-free bulk bag opening pneumatic conveying machine has emerged as a critical solution. This technology combines advanced engineering with practical application to ensure that powder materials are transferred from bulk bags to processing equipment without the risk of contamination or environmental impact. In this article, we explore the fundamental principles behind these machines and highlight their key working scene characteristics, providing insights into how they enhance operational efficiency and safety in various industrial settings.

Company Overview: HeadPowder Engineering
HeadPowder Engineering, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced powder handling equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient bulk material handling solutions. HeadPowder Engineering's products are engineered to meet the stringent demands of modern manufacturing, ensuring durability, performance, and compliance with industry standards. The company's headquarters and manufacturing facilities are located in Shandong, China, where they leverage local expertise and resources to deliver cutting-edge solutions tailored to global market needs.
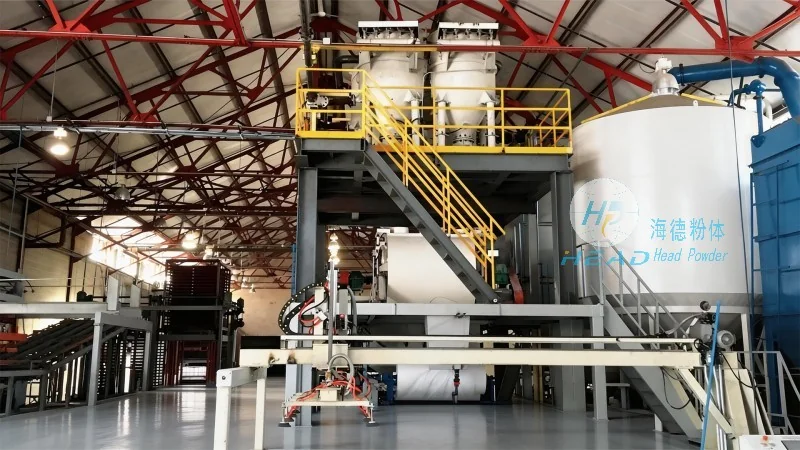
Principle of Operation for Dust-Free Bulk Bag Opening Pneumatic Conveying
The core principle of a dust-free bulk bag opening pneumatic conveying machine involves the controlled use of air pressure to transfer powder materials from a bulk bag into a processing system. The process begins with the opening of the bulk bag, which is typically sealed with a discharge spout or valve. A vacuum or pressure system is then activated to draw the powder from the bag and transport it through a pipeline to the receiving equipment. The machine is designed to minimize dust generation and ensure that the powder is handled in a contained environment, reducing the risk of airborne contamination and improving workplace safety. Key components include the bulk bag discharger, air filtration system, conveying pipeline, and receiving hopper or silo. The system operates by creating a pressure differential between the bag and the receiving container, ensuring that the powder flows smoothly and efficiently without clogging or loss. The dust-free design incorporates features such as sealed bag openings, air filtration, and enclosed conveying paths to maintain a clean and safe working environment.

Key Working Scene Characteristics and Applications
The dust-free bulk bag opening pneumatic conveying machine is particularly suited for applications in industries where powder purity and environmental control are paramount. Common working scene characteristics include high-volume material handling, need for minimal dust exposure, and integration with automated processing lines. Industries such as pharmaceuticals, food processing, chemical manufacturing, and cosmetics often rely on these systems to handle sensitive materials that cannot be exposed to contaminants or moisture. For example, in pharmaceutical manufacturing, the machine ensures that active ingredients are transferred without cross-contamination, maintaining product quality and regulatory compliance. In food processing, it prevents the introduction of foreign particles or bacteria into the product stream, enhancing food safety standards. The machine's ability to handle a wide range of powder types, from fine powders to bulkier granules, makes it versatile for various applications. Additionally, its compact design allows for integration into existing production lines without significant modifications, reducing downtime and operational costs.
Technical Advantages and Benefits in Industrial Settings
Implementing a dust-free bulk bag opening pneumatic conveying machine offers several technical advantages that enhance operational efficiency and safety. One of the primary benefits is the reduction of dust exposure, which not only improves worker health and safety but also minimizes the risk of product contamination. The enclosed conveying system prevents dust from escaping into the environment, making it compliant with environmental regulations and reducing cleanup efforts. Another advantage is the increased material handling capacity, as these machines can transfer large quantities of powder quickly and efficiently, reducing the need for manual handling and associated labor costs. The system's automation capabilities also contribute to improved process control, allowing for consistent material flow and reduced variability in product quality. Furthermore, the machine's durability and low maintenance requirements ensure long-term reliability, minimizing downtime and maintenance expenses. The integration of advanced control systems enables real-time monitoring of the conveying process, allowing operators to adjust parameters as needed to optimize performance. This level of control enhances overall operational efficiency and ensures that the system operates at peak performance.

Conclusion and Company Contact Information
In conclusion, the dust-free bulk bag opening pneumatic conveying machine is a vital technology for industries requiring efficient, clean, and safe handling of bulk powders. By combining advanced engineering with practical application, these machines enhance operational efficiency, improve workplace safety, and maintain product quality. HeadPowder Engineering, with its expertise and commitment to quality, provides reliable solutions tailored to the needs of various industrial sectors. Based in Shandong, China, the company leverages local resources and global standards to deliver cutting-edge powder handling equipment that meets the evolving demands of modern manufacturing. For businesses seeking to improve their bulk material handling processes, the dust-free bulk bag opening pneumatic conveying machine from HeadPowder Engineering represents a robust and effective solution.




