For industrial applications involving the transportation of stone coal material, pneumatic conveying systems offer an efficient and reliable solution. This equipment is designed to handle bulk materials like stone coal, ensuring smooth and continuous material transfer within processing facilities. The following sections will delve into the working principle and key features of such equipment, providing a comprehensive understanding of its functionality and advantages. As a specialized manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder) has developed advanced solutions tailored to the unique requirements of stone coal material handling.
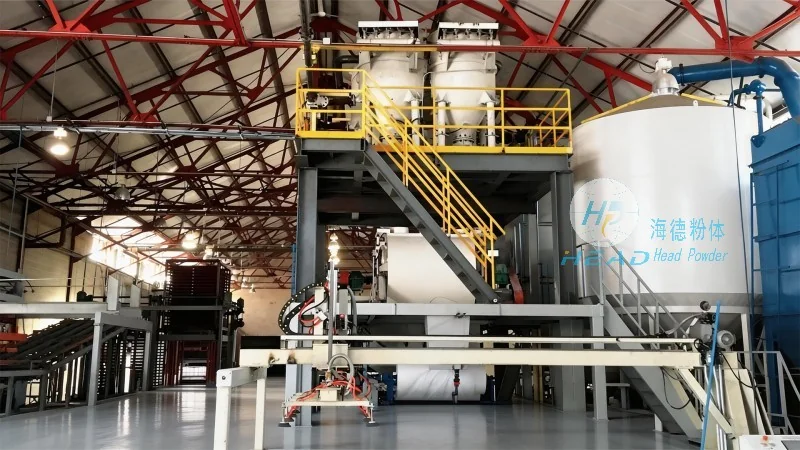
Working Principle of Pneumatic Conveying Systems for Stone Coal Material
The core mechanism of a stone coal material pneumatic conveying machine involves the use of compressed air to transport solid particles through a pipeline. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a duct or pipeline. Compressed air, generated by a blower or fan, is introduced into the system, creating a flow that propels the material forward. The air velocity within the pipeline is carefully controlled to ensure that the material is carried without causing excessive wear or degradation. The system may include components such as a separator, where the material is separated from the air stream, and a collection tank or silo for the material to be discharged. The entire process is automated, allowing for consistent and efficient material handling, with minimal human intervention required. The design of the system ensures that the material is transported in a controlled manner, maintaining its integrity and preventing contamination. This is particularly important for stone coal material, which may have specific handling requirements to avoid breakage or loss of quality.
Key Features and Advantages of Stone Coal Material Pneumatic Conveying Equipment
Several notable features distinguish pneumatic conveying systems for stone coal material from traditional mechanical conveyors. Firstly, the equipment offers a high degree of flexibility in terms of layout and installation, as it can be configured to follow the existing infrastructure of a facility. This adaptability allows for the integration of the system into existing processing lines without major modifications. Secondly, the system provides excellent dust control, as the material is enclosed within the pipeline, preventing dust emissions and maintaining a clean working environment. This is a significant advantage in industrial settings where air quality and worker safety are critical. Additionally, the equipment is capable of handling a wide range of material sizes and densities, making it suitable for various applications in the stone coal industry. Whether dealing with fine or coarse particles, the system can be adjusted to optimize performance. Another key advantage is the reduced maintenance requirements compared to mechanical systems, as there are fewer moving parts and less wear on components. This translates to lower operational costs and less downtime for maintenance. The system also offers energy efficiency, as the compressed air can be optimized to minimize energy consumption while maintaining optimal material transport. Advanced control systems allow for real-time monitoring and adjustment of air pressure and flow, ensuring energy savings without compromising performance. Furthermore, the equipment is designed for durability and longevity, with robust construction to withstand the demands of continuous operation in industrial settings. High-quality materials and precision manufacturing ensure that the system can operate reliably for extended periods, providing a long service life.

Customization and Application Flexibility
HeadPowder recognizes that each industrial facility has unique requirements when it comes to material handling. Therefore, the company offers customized solutions for stone coal material pneumatic conveying equipment. This includes the ability to adjust the system's capacity, pressure, and layout to match the specific needs of the application. Whether the facility requires a low-capacity system for small-scale operations or a high-capacity system for large-scale processing, HeadPowder can provide tailored solutions. The company also considers factors such as the material's physical properties, such as moisture content and abrasiveness, when designing the system. This ensures that the equipment is optimized for the specific characteristics of the stone coal material being handled. Additionally, the system can be integrated with other processing equipment, such as crushers, screens, or storage silos, to create a comprehensive material handling solution. This integration enhances overall efficiency and reduces the need for manual intervention in the material flow process.

Quality Assurance and Reliability
Shandong HeadPowder Engineering Co., Ltd. places a strong emphasis on quality assurance throughout the manufacturing process. Each component of the pneumatic conveying system is manufactured using high-quality materials and precision engineering techniques. The company adheres to strict quality control standards to ensure that every product meets or exceeds industry specifications. This commitment to quality is reflected in the durability and reliability of the equipment. HeadPowder's systems are designed to operate continuously without frequent breakdowns, minimizing downtime and maximizing productivity. The company also provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that clients can maintain the optimal performance of their equipment. This support is particularly important for industrial facilities that rely on consistent material supply and processing efficiency.
Conclusion
Stone coal material pneumatic conveying equipment, as provided by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated and efficient solution for industrial material handling. By leveraging the principles of pneumatic transport, the equipment offers numerous advantages over traditional mechanical systems, including flexibility, dust control, and reduced maintenance. The working principle, which involves the use of compressed air to transport material through a pipeline, is designed to handle the unique characteristics of stone coal material, ensuring minimal degradation and consistent performance. With its focus on customization, quality, and reliability, HeadPowder has established itself as a trusted provider in the industry. The company's solutions are tailored to meet the specific needs of clients, ensuring that they can achieve optimal material handling efficiency while maintaining a safe and clean working environment. As industrial demands continue to evolve, the advanced capabilities of pneumatic conveying systems will remain a critical component in the processing of stone coal material, and HeadPowder is positioned to provide the innovative solutions needed to meet these challenges.




