For industrial applications involving the transport of rubber granules, efficient and reliable pneumatic conveying systems are essential. This article provides an overview of rubber granule pneumatic conveying systems, detailing their structural components and operational principles. The system is designed to handle rubber granules with precision, ensuring minimal product degradation and optimal performance in various industrial settings.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design and production of pneumatic conveying equipment. With a focus on quality and innovation, the company serves a wide range of industries, including rubber processing, chemical manufacturing, and food processing. HeadPowder's expertise lies in developing customized solutions tailored to the unique requirements of each client, ensuring efficient material handling and enhanced operational efficiency.
Structural Components of Rubber Granule Pneumatic Conveying Systems
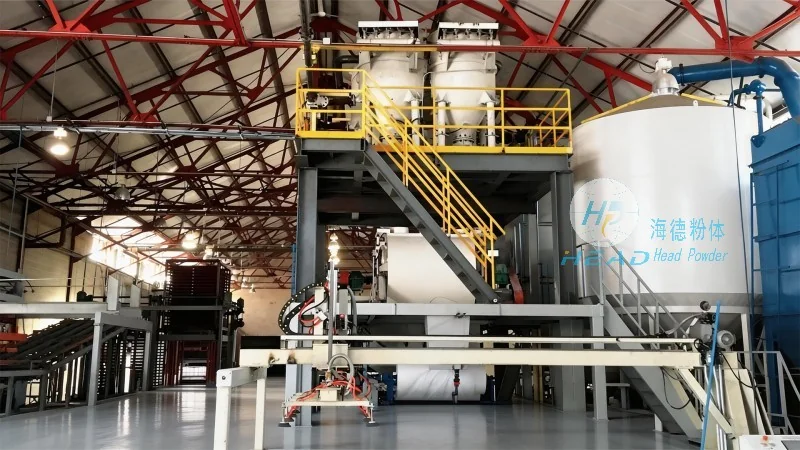
The rubber granule pneumatic conveying system typically consists of several key components that work in tandem to achieve effective material transport. These components include the hopper, which serves as the storage and feeding unit for the rubber granules; the air compressor, responsible for generating the necessary air pressure to move the material; the conveying line, which may be composed of flexible hoses or rigid pipes; and the receiver, where the material is deposited after transport. Each component is engineered to withstand the specific demands of rubber granule handling, ensuring durability and long-term performance.

Working Principles of the Pneumatic Conveying System
The operation of the rubber granule pneumatic conveying system relies on the principles of air movement and material suspension. When the air compressor is activated, it generates a high-pressure air stream that enters the conveying line. The rubber granules are then introduced into the system, typically via the hopper, and are entrained by the air flow. The air stream lifts and transports the granules through the conveying line to the receiver. The system maintains a consistent air pressure and flow rate to ensure smooth and continuous material transport, minimizing the risk of blockages or product degradation.

Advantages of Rubber Granule Pneumatic Conveying Systems
Implementing a rubber granule pneumatic conveying system offers several advantages for industrial operations. These systems provide a dust-free and hygienic method of material transport, which is particularly important in food and pharmaceutical industries. Additionally, pneumatic conveying systems are capable of handling abrasive materials like rubber granules without causing excessive wear on equipment components. The flexibility of the system allows for easy integration into existing production lines, and the ability to transport materials over long distances without the need for intermediate storage points enhances overall operational efficiency.
Conclusion
Rubber granule pneumatic conveying systems, as offered by Shandong HeadPowder Engineering Co., Ltd., represent a reliable and efficient solution for material handling in various industrial applications. By understanding the structural components and operational principles of these systems, industries can optimize their material transport processes, reduce operational costs, and enhance overall productivity. HeadPowder's commitment to quality and innovation ensures that clients receive tailored solutions that meet their specific needs, contributing to long-term success in their respective fields.




