HeadPowder, a leading enterprise in the field of powder processing technology, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems for nanometer calcium carbonate. This article provides a detailed overview of the operation process and working principle of our nanometer calcium carbonate pneumatic conveying equipment, highlighting its efficiency, reliability, and industrial applications.

Overview of Nanometer Calcium Carbonate Pneumatic Conveying Equipment
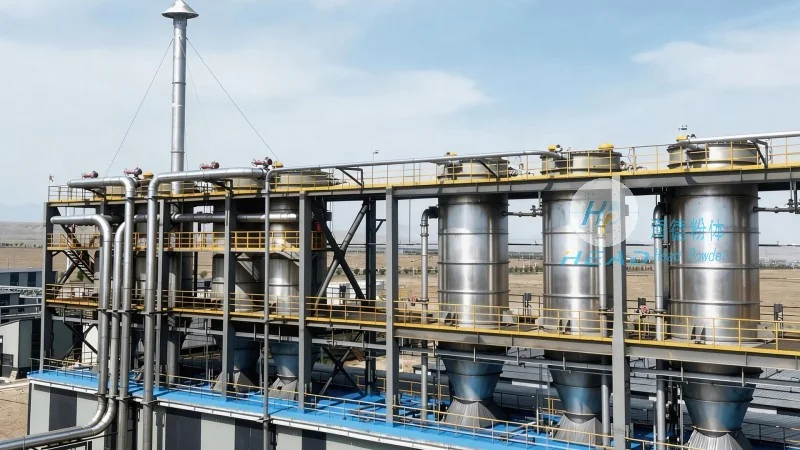
The nanometer calcium carbonate pneumatic conveying equipment is engineered to handle fine powders with high precision and minimal particle degradation. This system is particularly suitable for industrial applications where the transport of nanoscale calcium carbonate particles requires controlled velocity, low pressure, and efficient separation. The equipment is designed to meet the stringent quality standards of modern manufacturing processes, ensuring consistent product quality and operational safety.
Key Components and Their Functions
The pneumatic conveying system for nanometer calcium carbonate typically consists of several critical components that work in tandem to achieve seamless material transport. These include the hopper for material storage, the air compressor or blower for generating the conveying air, the pipeline system for transporting the powder-air mixture, the control valves for regulating flow, and the dust collector or filter for maintaining air quality. Each component plays a vital role in optimizing the conveying process and ensuring the integrity of the nanometer calcium carbonate particles.

Working Principle of the Pneumatic Conveying Process
The operation of the nanometer calcium carbonate pneumatic conveying equipment is based on the principle of pneumatic transport, where the powder is suspended and transported by a stream of air. The process begins with the material being fed from the hopper into the conveying line. Simultaneously, the air compressor generates a high-pressure air stream that is introduced into the pipeline. As the air flows through the line, it creates a low-pressure zone that draws the calcium carbonate particles into the air stream, forming a dense phase or dilute phase mixture depending on the system design. The mixture then travels through the pipeline to the destination point, such as a storage silo or processing unit. At the receiving end, the air is separated from the powder through a cyclone or filter, allowing the calcium carbonate to be discharged while the air is recirculated or discharged to the atmosphere. This closed-loop system minimizes material loss and ensures efficient use of energy.
Operation Process: Step-by-Step Guide
The operation of the nanometer calcium carbonate pneumatic conveying equipment follows a systematic process to ensure smooth and continuous material transport. The steps are as follows:

- Material Loading: The hopper is filled with nanometer calcium carbonate powder, and the level is monitored to prevent overfilling. The material is then released into the conveying line via a feeder, such as a rotary valve or screw feeder, which controls the flow rate.
- Air Supply Initiation: The air compressor is started, and the air pressure is adjusted to the required level. The blower or compressor generates a steady flow of air that is directed into the pipeline. The pressure and flow rate are monitored to maintain optimal conveying conditions.
- Powder Conveying: As the air flows through the pipeline, it lifts the calcium carbonate particles into the air stream. The mixture travels through the pipeline to the destination point. The velocity of the air is carefully controlled to prevent particle degradation and ensure uniform transport.
- Material Discharge: At the receiving end, the air and powder mixture enters a separation unit, such as a cyclone separator. The centrifugal force in the cyclone separates the powder from the air. The separated calcium carbonate is collected in a container or silo, while the air is either filtered and recirculated or released to the environment.
- System Shutdown: When the conveying operation is complete, the air compressor is turned off, and the system is depressurized. The feeder is stopped, and the hopper is emptied. The system is then cleaned and maintained as per the manufacturer's guidelines to ensure longevity and performance.
Advantages of Using Nanometer Calcium Carbonate Pneumatic Conveying Equipment
Implementing a pneumatic conveying system for nanometer calcium carbonate offers several advantages over traditional mechanical conveying methods. These benefits include:
- Reduced Material Degradation: The low-velocity, low-pressure conveying process minimizes the impact and friction on the fine particles, preserving their nanoscale structure and quality.
- Efficient and Compact Design: The system is compact and requires less floor space compared to traditional bulk handling equipment, making it suitable for industrial settings with limited space.
- Low Maintenance and Operational Costs: The pneumatic conveying system has fewer moving parts compared to mechanical conveyors, resulting in lower maintenance requirements and reduced operational costs over time.
- Enhanced Safety and Environmental Control: The closed-loop system with dust collection and air filtration minimizes dust emissions, ensuring a safe working environment and compliance with environmental regulations.
- Flexibility in Transport: The system can be easily integrated with existing processing lines and can transport materials over long distances with minimal loss and consistent quality.
Applications and Industries
The nanometer calcium carbonate pneumatic conveying equipment is widely used in various industries that rely on high-quality calcium carbonate for their products. Some of the key applications include:
- Paper and Pulp Industry: Nanometer calcium carbonate is used as a filler and coating agent in paper production, enhancing the paper's strength, brightness, and smoothness.
- Plastics and Rubber Industry: The fine particles are added to plastic and rubber compounds to improve their mechanical properties, such as tensile strength and impact resistance.
- Paint and Coatings Industry: Calcium carbonate is used as a pigment and extender in paints, providing opacity and reducing the cost of the coating.
- Construction Materials Industry: The powder is used in the production of cement, concrete, and other building materials, improving their durability and workability.
- Pharmaceutical and Food Industry: In these industries, the nanometer calcium carbonate is used as a filler or excipient, ensuring consistent particle size and quality for pharmaceutical formulations and food products.
Conclusion
HeadPowder's nanometer calcium carbonate pneumatic conveying equipment represents a cutting-edge solution for the efficient and reliable transport of fine powders in industrial applications. By understanding the operation process and working principle of this equipment, users can optimize their material handling processes, enhance product quality, and reduce operational costs. With its robust design, advanced technology, and commitment to quality, HeadPowder continues to be a trusted partner in providing innovative powder processing solutions to industries worldwide.




