Intelligent centralized pneumatic conveying equipment represents a sophisticated solution in material handling, designed to efficiently transport bulk materials over long distances with minimal human intervention. This technology integrates advanced automation and control systems, enabling precise management of material flow, pressure, and system performance. As a key component in modern industrial operations, such equipment enhances productivity while reducing operational costs and environmental impact. The design of these systems is tailored to meet diverse industrial needs, from pharmaceuticals and food processing to chemical and mining applications, ensuring compliance with stringent safety and hygiene standards.

Core Components and System Architecture
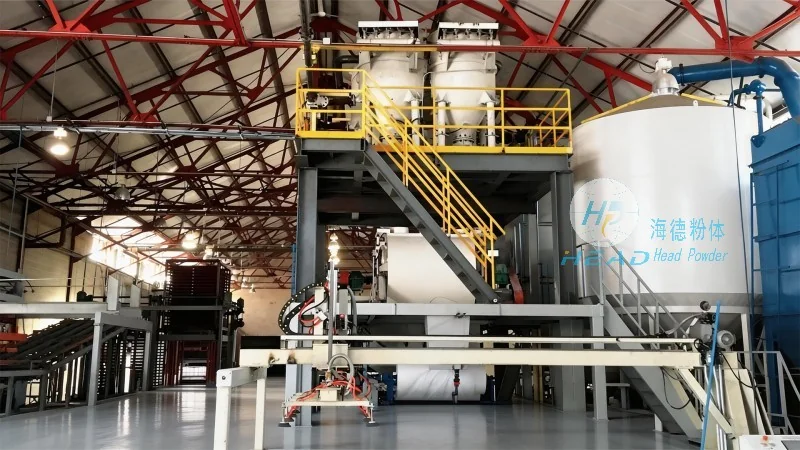
The intelligent centralized pneumatic conveying system typically comprises several critical components, each playing a vital role in the overall operation. The primary elements include a material feeding unit, a conveying pipeline network, a control system with sensors and actuators, and a receiving hopper or storage tank. The feeding unit, often equipped with a rotary valve or screw feeder, ensures consistent material supply into the system. The pipeline network, constructed from high-quality materials like stainless steel or aluminum, is designed to withstand the pressures and temperatures associated with pneumatic conveying. The control system, utilizing programmable logic controllers (PLCs) and advanced software, monitors real-time parameters such as pressure, flow rate, and material level, allowing for automated adjustments and fault detection. Sensors, including pressure transducers, flow meters, and level detectors, provide critical data to the control system, ensuring optimal performance and preventing system failures.

Operation Process: Step-by-Step Overview
The operation of intelligent centralized pneumatic conveying equipment follows a systematic sequence of steps, ensuring efficient material transport from the source to the destination. The process begins with the material being fed into the system via the feeding unit. The material is then drawn into the conveying pipeline by a vacuum or pressure source, depending on the system configuration. As the material travels through the pipeline, it is propelled by the air flow, which can be generated by a blower or compressor. The control system continuously monitors the system's performance, adjusting the air flow rate and pressure as needed to maintain consistent material transport. At the receiving end, the material is deposited into a hopper or storage tank, where it is then transferred to the next stage of the production process. The entire operation is automated, with the control system managing all aspects of the process, from start to finish. This automation not only improves efficiency but also reduces the risk of human error and ensures consistent material quality.
Working Principle: How It Works
The working principle of intelligent centralized pneumatic conveying equipment is based on the physics of fluid dynamics and material transport. The system operates by creating a pressure differential between the feeding point and the receiving point, which propels the material through the pipeline. In a vacuum system, the blower creates a low-pressure environment, drawing material from the source into the pipeline. In a pressure system, the compressor generates high-pressure air, pushing the material through the pipeline. The material is suspended in the air stream, moving along the pipeline with the air flow. The velocity of the air and the size of the particles determine the conveying capacity and efficiency of the system. The control system optimizes these parameters to ensure that the material is conveyed at the desired rate, minimizing energy consumption and maximizing throughput. The system also incorporates safety features, such as pressure relief valves and emergency stop buttons, to prevent accidents and protect personnel and equipment.
Advantages and Applications
Intelligent centralized pneumatic conveying equipment offers numerous advantages over traditional material handling methods. These include increased efficiency, reduced labor costs, improved material quality, and enhanced safety. The automation of the system minimizes the need for manual handling, reducing the risk of workplace injuries and improving product consistency. The system also reduces material waste and environmental impact by minimizing dust and spillage during transport. The equipment is highly versatile and can be adapted to various industrial applications, including the transportation of powders, granules, and bulk solids. In the pharmaceutical industry, for example, such equipment is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. In the food industry, it is used to convey ingredients like flour, sugar, and spices, ensuring compliance with food safety regulations. In the chemical industry, it is used to transport chemicals and reagents, providing a safe and efficient method of material handling.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of intelligent centralized pneumatic conveying equipment. The company is headquartered in Shandong, China, and has a strong reputation for delivering high-quality, reliable, and efficient material handling solutions. HeadPowder's team of experienced engineers and technicians specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of each client. The company's products are known for their advanced technology, robust construction, and excellent performance, making them suitable for a wide range of industrial applications. HeadPowder is committed to providing exceptional customer service, including installation, maintenance, and technical support, to ensure that clients receive the best possible service and support throughout the life of their equipment. The company's dedication to quality and innovation has made it a trusted partner for many industries, helping them to improve their operational efficiency and achieve their business goals.




