Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of material handling solutions, specializes in the design, manufacturing, and application of advanced equipment for transporting maltose and related materials. This article delves into the fundamental principles and distinctive working scene characteristics of maltose material handling systems, providing a comprehensive overview of their operational mechanisms and practical applications.

The Principle of Maltose Material Handling System Equipment
The maltose material handling system is engineered to efficiently transport maltose, a crucial ingredient in the food and beverage industry, from production lines to storage or processing areas. The core components typically include conveyor belts, feeding mechanisms, control systems, and safety features, all integrated to ensure smooth and reliable material flow. The system operates on the principle of mechanical energy conversion, where motor-driven components move the material along designated paths. For instance, belt conveyors use friction to move the maltose, while screw conveyors utilize rotational motion to push the material forward. The control system, often equipped with sensors and programmable logic controllers (PLCs), monitors the flow rate, temperature, and other critical parameters to maintain optimal performance and prevent blockages or overloads.

Working Scene Characteristics of Maltose Material Handling Systems
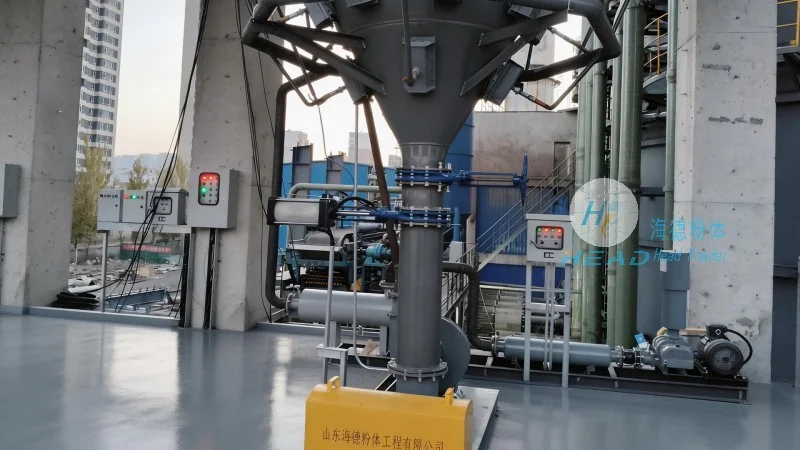
The working scene characteristics of maltose material handling systems are tailored to the specific demands of maltose production and processing environments. These systems are designed to handle the unique properties of maltose, such as its granular or powdered form, and the need for hygienic and contamination-free handling. In industrial settings, the equipment is often installed in clean rooms or enclosed areas to minimize dust and maintain product purity. The systems are also built to withstand the moisture and temperature variations common in maltose processing, ensuring consistent material quality. Additionally, the working scene characteristics include high efficiency and low maintenance requirements, as the equipment is engineered for continuous operation with minimal downtime. The systems are adaptable to different production scales, from small-scale batches to large-scale industrial operations, making them suitable for various applications, including food manufacturing, pharmaceuticals, and chemical processing.
Application Scenarios in Maltose Production
In the context of maltose production, the material handling system plays a vital role in ensuring the smooth flow of raw materials and finished products. For example, in a maltose manufacturing plant, the system may start with receiving maltose from suppliers, where a receiving hopper and conveyor belt transport the material into the production line. The system then moves the maltose through various processing stages, such as mixing, drying, and packaging, using different types of conveyors and feeding mechanisms. The working scene characteristics in this scenario include the need for precise control over material flow to avoid clogging in the drying equipment or overloading the packaging machines. The system is also designed to handle the high volume of maltose produced, with the ability to adjust the conveyor speed based on production demand. Furthermore, the hygienic design of the equipment ensures that the maltose remains free from contaminants, which is critical for meeting food safety regulations and maintaining product quality.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality maltose material handling solutions that meet the evolving needs of the industry. With years of experience and a team of skilled engineers, the company offers customized equipment tailored to specific production requirements. The company's headquarters is located in Shandong, China, and it serves clients globally with its reliable and efficient material handling systems. By focusing on innovation and customer satisfaction, HeadPowder continues to be a trusted partner in the maltose processing industry.




