Organic salt, a critical component in numerous industrial processes, demands efficient and reliable transportation methods to maintain operational efficiency. The organic salt pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder) addresses these requirements with advanced engineering and robust design, offering a solution that enhances productivity and safety in material handling operations.

Company Overview
HeadPowder, a leading provider of material handling solutions, specializes in designing and implementing innovative pneumatic conveying systems. With a strong operational base in Shandong, China, the company has established a reputation for delivering high-quality equipment tailored to diverse industrial needs. The company’s commitment to excellence is reflected in its state-of-the-art facilities and a team of experienced professionals dedicated to ensuring customer satisfaction and system reliability.
Key Features of the Organic Salt Pneumatic Conveying Solution
The organic salt pneumatic conveying system from headpowder is engineered to handle organic salt with precision and efficiency. Key features include:
1. Customized Conveying Design: The system is designed to accommodate various particle sizes and flow rates of organic salt, ensuring optimal performance under different operational conditions. This customization allows for seamless integration into existing production lines or as a standalone solution.
2. Advanced Material Handling Technology: Utilizing high-pressure air or vacuum systems, the conveying process is gentle yet effective, minimizing product degradation and preserving the integrity of the organic salt. The system incorporates advanced control mechanisms that enable real-time monitoring and adjustment of conveying parameters.
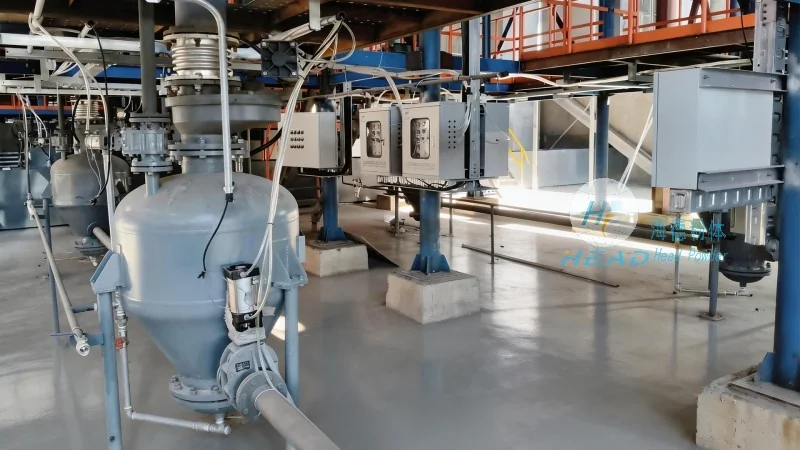
3. Robust Construction and Durability: Built with high-quality materials, the equipment is designed to withstand the corrosive nature of organic salt and the demands of continuous operation. This durability ensures long-term reliability and reduces maintenance costs over the system's lifespan.
4. Energy Efficiency and Environmental Compliance: The system incorporates energy-saving features, such as optimized air consumption and efficient filtration systems, to minimize operational costs while adhering to environmental regulations. This focus on sustainability aligns with modern industrial standards and client expectations.
Application Scenarios
The organic salt pneumatic conveying solution is applicable across a wide range of industries where organic salt is a key raw material. These include:
1. Chemical Manufacturing: In chemical plants, the system efficiently transports organic salt to reactors and processing units, ensuring consistent supply and reducing downtime.

2. Food Processing: For food-grade organic salt applications, the system maintains hygiene standards and prevents contamination, making it suitable for production lines that require strict quality control.
3. Pharmaceutical Industry: In pharmaceutical manufacturing, the conveying system ensures that organic salt is handled in a sterile and controlled environment, meeting regulatory requirements for drug production.
4. Industrial Production Lines: The system can be integrated into larger production lines to facilitate the movement of organic salt between different stages of processing, enhancing overall operational efficiency.
Benefits for Clients
Implementing the organic salt pneumatic conveying system from headpowder offers numerous advantages to clients, including:
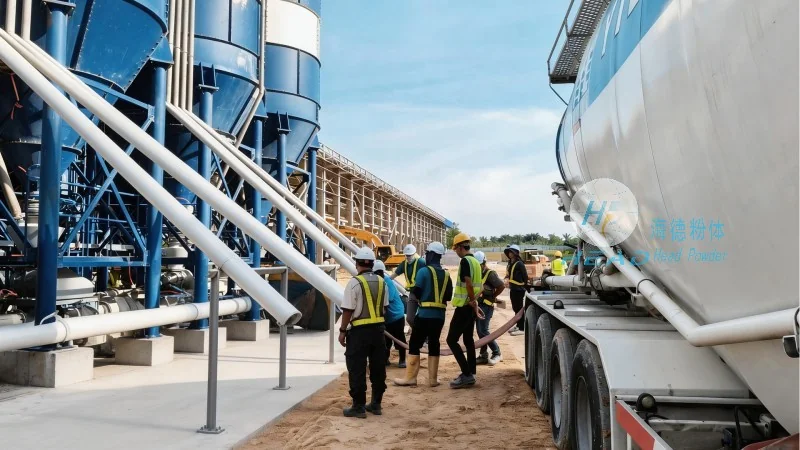
1. Increased Productivity: The efficient conveying process reduces material handling time and minimizes bottlenecks in production, leading to higher output and improved operational efficiency.
2. Enhanced Safety: By eliminating manual handling of organic salt, the system reduces the risk of accidents and exposure to hazardous materials, creating a safer working environment.
3. Cost Savings: The energy-efficient design and reduced maintenance requirements contribute to lower operational costs over the long term. Additionally, the system's durability minimizes replacement and repair expenses.
4. Improved Product Quality: The gentle handling of organic salt by the system preserves its quality and prevents degradation, ensuring that the final product meets or exceeds industry standards.




