For industries dealing with magnesium sulfate, efficient material handling is crucial. A pneumatic conveyor system designed specifically for this application offers a reliable solution that combines performance with operational advantages. This article explores the working principle and key features of a magnesium sulfate material pneumatic conveyor, highlighting how such equipment enhances productivity and safety in material transport processes.

Working Principle of Magnesium Sulfate Pneumatic Conveyors
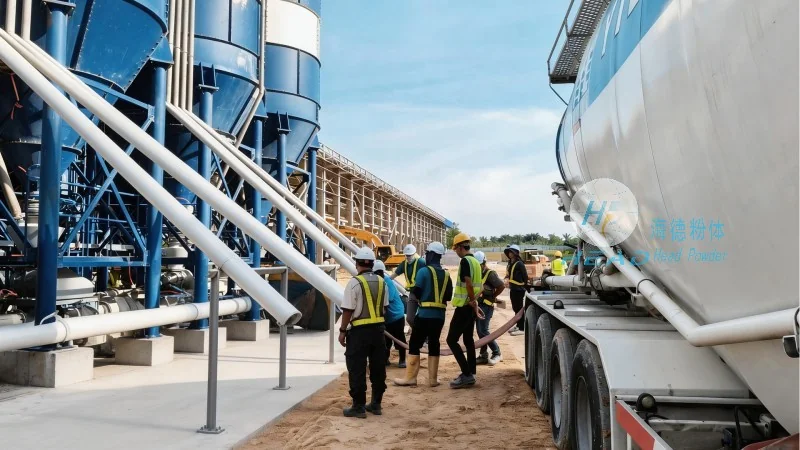
The core of a magnesium sulfate pneumatic conveyor lies in its air-driven mechanism. The system operates by using compressed air to create a flow that transports the material through a pipeline. As the material is introduced into the system, it is carried by the air stream, moving from the inlet to the discharge point. The design typically includes a hopper for material storage, a rotary valve or feeder to control the flow rate, and a series of pipes that form the conveying path. The air pressure and flow rate are carefully regulated to ensure the material is transported without degradation or blockage. This air-driven approach eliminates the need for mechanical components that might cause wear or maintenance issues, making it suitable for handling fine or abrasive materials like magnesium sulfate.
Key Features of Magnesium Sulfate Pneumatic Conveyors
Several distinct features make magnesium sulfate pneumatic conveyors an ideal choice for material handling. First, the system provides a dust-free and enclosed transport environment, which is essential for maintaining product quality and safety standards. The enclosed design prevents contamination and exposure to airborne particles, which is particularly important for magnesium sulfate, as it can be a respiratory irritant. Second, the flexibility of the system allows for easy integration into existing production lines. The conveyor can be configured to handle various distances and layouts, adapting to the specific needs of the facility. Third, the low maintenance requirements contribute to operational efficiency. Unlike traditional belt or screw conveyors, pneumatic systems have fewer moving parts, reducing the risk of breakdowns and the need for frequent repairs. Additionally, the ability to handle both dry and slightly moist materials without clogging is a significant advantage, as magnesium sulfate can sometimes have a tendency to clump under certain conditions. The system's ability to maintain consistent flow rates also ensures that the production process remains stable and predictable.
Benefits of Using a Magnesium Sulfate Pneumatic Conveyor
Implementing a magnesium sulfate pneumatic conveyor brings numerous benefits to industrial operations. One of the primary advantages is the improvement in workplace safety. By containing the material within the system, the risk of dust exposure and inhalation is minimized, creating a healthier working environment. This is particularly important in facilities where magnesium sulfate is processed in large quantities. Another benefit is the enhancement of product quality. The enclosed transport prevents contamination from external sources, ensuring that the material remains pure and meets the required specifications. This is critical for applications where magnesium sulfate is used in pharmaceuticals, food additives, or chemical manufacturing, where purity is paramount. Furthermore, the system's ability to handle high volumes efficiently reduces processing time and increases overall productivity. The consistent flow and reduced downtime due to maintenance make it a cost-effective solution in the long run. The energy efficiency of pneumatic systems, as they use compressed air rather than mechanical power, also contributes to lower operational costs. Finally, the adaptability of the conveyor allows for easy expansion or modification as production needs change, providing a scalable solution for growing businesses.

Applications and Industries Using Magnesium Sulfate Pneumatic Conveyors
Magnesium sulfate pneumatic conveyors are widely used across various industries that rely on this material. In the chemical industry, they are essential for transporting magnesium sulfate from storage to processing units, ensuring a smooth flow of raw materials. The pharmaceutical sector benefits from the system's ability to maintain product purity, as any contamination could compromise the effectiveness of medications. The food industry, particularly in the production of baking powders and other food additives, uses these conveyors to handle magnesium sulfate safely and efficiently. Additionally, in the agricultural sector, where magnesium sulfate is used as a fertilizer, the system aids in the distribution of the material to farms. The versatility of the conveyor makes it suitable for both large-scale industrial operations and smaller-scale applications, such as in research laboratories or small-scale manufacturing facilities.
Conclusion and Company Information
Overall, a magnesium sulfate material pneumatic conveyor is a sophisticated and efficient solution for material handling. Its working principle, based on air-driven transport, offers numerous advantages over traditional methods, including improved safety, product quality, and operational efficiency. The key features, such as enclosed transport and low maintenance, make it a reliable choice for industries dealing with magnesium sulfate. By choosing a pneumatic conveyor from Shandong HeadPowder Engineering Co., Ltd., businesses can enhance their material handling processes and achieve better results. With a focus on quality and innovation, HeadPowder provides systems that are tailored to the specific needs of each client, ensuring optimal performance and long-term satisfaction. Based in Shandong, China, HeadPowder Engineering Co., Ltd. is committed to delivering high-quality equipment that meets the demands of modern industrial applications.




