For industries dealing with sodium dithionite, an efficient and reliable material handling solution is crucial. The pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. (headpowder) offers a sophisticated approach to transporting this chemical efficiently and safely. This article explores the working principle and key features of this specialized system.

Introduction to the Pneumatic Conveying System for Sodium Dithionite Materials
Sodium dithionite, also known as sodium hydrosulfite, is widely used in various industrial processes, including bleaching, reduction, and as a reducing agent. Handling this material requires careful consideration due to its hygroscopic nature and potential reactivity. The pneumatic conveying system developed by headpowder addresses these challenges by providing a closed-loop, dust-free, and energy-efficient method for material transport. The system is engineered to meet the specific demands of sodium dithionite, ensuring minimal product degradation and optimal operational performance.

Working Principle of the System
The core of the pneumatic conveying system is the air-driven mechanism that transports sodium dithionite particles through a network of pipes. The process begins with the material being fed into a hopper or feeder, where it is then introduced into a high-pressure air stream. The air, typically supplied by a blower or compressor, creates a flow that propels the material through the system. The system may employ different conveying modes, such as pressure or vacuum pneumatic conveying, depending on the application requirements. In pressure systems, the air is introduced at the inlet, while in vacuum systems, it is drawn from the outlet. The design ensures that the air velocity is sufficient to prevent particle settling and maintain a stable flow, minimizing the risk of blockages or material loss.

Key Features and Advantages
Several distinct features make the headpowder pneumatic conveying system ideal for sodium dithionite handling. Firstly, the system operates in a closed environment, which prevents exposure to moisture and contaminants, preserving the material's quality and shelf life. This is particularly important for sodium dithionite, which is sensitive to humidity and can degrade if exposed to air for extended periods. Secondly, the system is highly efficient in terms of energy consumption, as it minimizes the need for manual handling and reduces the risk of product spillage. The closed-loop design also contributes to environmental sustainability by reducing dust emissions and improving workplace safety. Additionally, the system is designed for easy maintenance and scalability, allowing it to adapt to changing production needs without significant modifications.
Technical Specifications and Application Scenarios
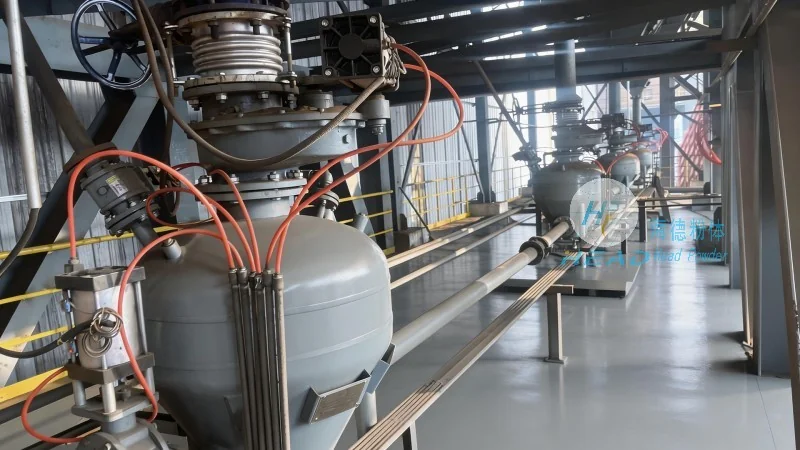
The pneumatic conveying system from headpowder is equipped with advanced components tailored to sodium dithionite's properties. The system typically includes a hopper with a level indicator, a feeder with adjustable flow control, a blower or compressor for air supply, and a series of pipes with appropriate diameters and bends. The air velocity is carefully controlled to ensure the material is conveyed at an optimal speed, avoiding excessive wear on the equipment and minimizing energy usage. The system can handle various particle sizes and flow rates, making it suitable for both small-scale and large-scale production facilities. Applications include material transfer between storage silos, processing units, and packaging lines, as well as integration with existing production systems to enhance overall efficiency.
Company Profile and Service Commitment
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for chemical industries. With a strong focus on innovation and customer satisfaction, the company has developed a range of products tailored to the unique needs of sodium dithionite and other chemicals. Headquartered in Shandong, China, the company leverages its local expertise and advanced manufacturing capabilities to deliver high-quality, reliable systems. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, ensuring that each system meets the highest performance and safety requirements. Customers benefit from comprehensive support, including design, installation, and after-sales service, to ensure long-term operational success.




