Ammonium bicarbonate, a widely used chemical in industrial applications, requires specialized handling systems to ensure safety, efficiency, and compliance with operational standards. The material handling systems designed for ammonium bicarbonate are engineered to address the unique properties of this substance, including its reactivity, dustiness, and the need for precise control during transport and processing. This article explores the working principles and key features of the equipment used in ammonium bicarbonate material handling systems, providing insights into how these systems enhance operational performance and safety.

Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of chemical processing equipment, specializes in the design, development, and production of material handling systems tailored to the needs of the chemical industry. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner for businesses requiring reliable equipment for handling ammonium bicarbonate and other similar chemicals. HeadPowder operates from Shandong, China, leveraging local expertise and advanced manufacturing capabilities to deliver high-quality products that meet international standards.
Introduction to Ammonium Bicarbonate Material Handling Systems
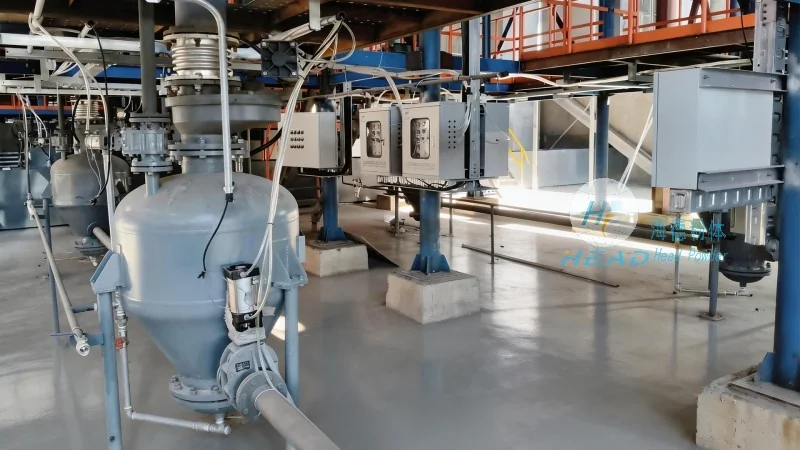
Ammonium bicarbonate material handling systems are sophisticated equipment designed to transport, store, and process ammonium bicarbonate efficiently and safely. These systems are critical in industries such as food processing, pharmaceuticals, and chemical manufacturing, where the accurate handling of this chemical is essential for product quality and operational safety. The systems typically include components like hoppers, conveyors, dust collectors, and control panels, all integrated to work in harmony to ensure smooth material flow and minimal risk of contamination or accidents.

Working Principle of Ammonium Bicarbonate Material Handling Equipment
The working principle of ammonium bicarbonate material handling systems revolves around the controlled movement of the material from its source to its destination. The process typically begins with the material being loaded into a hopper, where it is stored and prepared for transport. From the hopper, the material is then conveyed through a system of pipes or mechanical components, depending on the specific design of the equipment. For example, pneumatic conveying systems use air pressure to move the material, while mechanical conveyors rely on belts or screws to transport it. The control system, often integrated with sensors and automation technology, monitors the flow rate, pressure, and other parameters to ensure the material is handled under optimal conditions. This principle ensures that the material is moved with precision, minimizing the risk of spillage, dust generation, or other hazards associated with handling ammonium bicarbonate.
Key Features of Ammonium Bicarbonate Material Handling Systems
The features of ammonium bicarbonate material handling systems are tailored to address the specific challenges of handling this chemical. One of the primary features is the use of dust control mechanisms, such as enclosed systems and efficient dust collectors, to prevent the release of fine particles into the environment. This is crucial for maintaining air quality and ensuring compliance with environmental regulations. Another important feature is the integration of safety measures, including emergency stop buttons, pressure relief valves, and monitoring systems that alert operators to any abnormalities in the system. The systems also often include automation capabilities, allowing for remote control and monitoring, which enhances operational efficiency and reduces the need for manual intervention. Additionally, the equipment is designed for durability and ease of maintenance, with components that can withstand the corrosive and abrasive nature of ammonium bicarbonate, ensuring long-term reliability and low operational costs.
Efficiency and Performance in Ammonium Bicarbonate Handling
The efficiency of ammonium bicarbonate material handling systems is a critical factor in industrial operations. These systems are engineered to minimize downtime and maximize throughput, which directly impacts the productivity of the overall process. The use of advanced materials and manufacturing techniques ensures that the equipment can handle the abrasive and corrosive properties of ammonium bicarbonate without degradation over time. Furthermore, the integration of energy-efficient components, such as variable speed drives and optimized conveyor systems, reduces operational costs by minimizing energy consumption. The systems also feature easy access points for maintenance, allowing for quick repairs and replacements, which helps to maintain consistent performance and reduce maintenance-related downtime. Overall, the efficiency and performance of these systems contribute significantly to the economic viability of operations that rely on the handling of ammonium bicarbonate.
Conclusion: Advantages of Using Ammonium Bicarbonate Material Handling Systems
In conclusion, the working principles and features of ammonium bicarbonate material handling systems are designed to provide a safe, efficient, and reliable solution for handling this important chemical. The systems offered by Shandong HeadPowder Engineering Co., Ltd. leverage advanced technology and engineering expertise to address the unique challenges of ammonium bicarbonate processing. By incorporating dust control, safety measures, automation, and durable components, these systems enhance operational performance, reduce risks, and lower long-term costs. For industries requiring reliable equipment for ammonium bicarbonate handling, the systems from HeadPowder represent a superior choice that meets both current and future operational needs.




