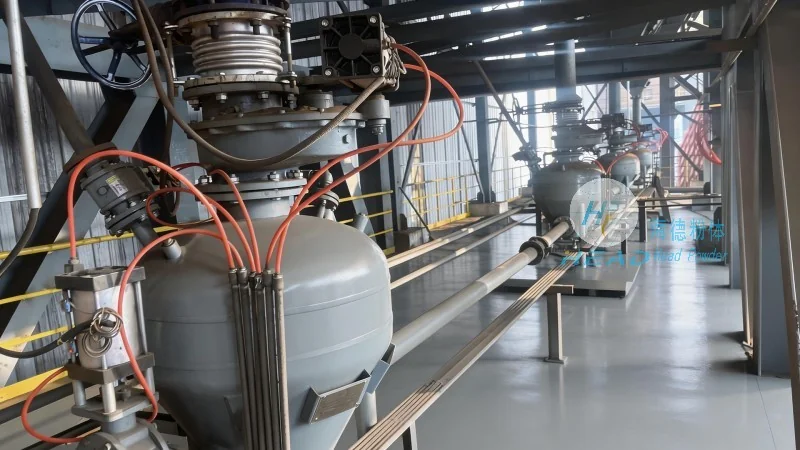
When it comes to efficiently transporting fertilizer powders, specialized equipment plays a crucial role in ensuring smooth operations and maintaining product integrity. The fertilizer powder conveying equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is designed to address the unique challenges associated with handling bulk powders in agricultural and industrial applications. This equipment is engineered to provide reliable and efficient solutions for the movement of fertilizer materials from storage to processing or distribution points.

The core working principle of this fertilizer powder conveying system revolves around the use of advanced pneumatic or mechanical technologies to move bulk powders through pipelines or conveyor systems. The system typically operates by creating a pressure differential or utilizing mechanical components such as screws, belts, or air pressure to transport the powder. For instance, pneumatic conveying systems use compressed air to draw or push the powder through a network of pipes, while mechanical systems rely on rotating components to move the material along a defined path. This dual approach ensures that the fertilizer powder is transported with minimal segregation and loss, preserving its quality and ensuring consistent delivery.

A key feature of the fertilizer powder conveying equipment from HeadPowder is its ability to handle a wide range of powder types, including granular, fine, and even cohesive materials. The design incorporates adjustable parameters such as air flow rate, pressure, and conveyor speed, allowing for customization based on the specific characteristics of the fertilizer being transported. This adaptability is crucial for optimizing performance and reducing operational costs. Additionally, the equipment is constructed with high-quality materials that are resistant to corrosion and wear, ensuring long-term durability and minimal maintenance requirements.

Another significant advantage is the system's energy efficiency. By optimizing the air flow and mechanical components, the conveying process consumes less energy compared to traditional methods like manual handling or bucket elevators. This not only reduces operational expenses but also aligns with sustainable practices in the agricultural sector. The equipment also features safety mechanisms, such as pressure relief valves and overload protection, to prevent accidents and ensure the well-being of operators.
From a practical standpoint, the fertilizer powder conveying equipment is easy to integrate into existing production lines. It can be installed in various configurations, including vertical, horizontal, or inclined setups, depending on the layout of the facility. The modular design allows for easy expansion or modification as production needs evolve. Furthermore, the system's compact footprint makes it suitable for both large-scale industrial facilities and smaller agricultural operations, providing flexibility across different scales of operation.
In summary, the fertilizer powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. combines advanced technology with robust engineering to deliver efficient, reliable, and cost-effective solutions for fertilizer transportation. By understanding the working principles and key features of this equipment, users can make informed decisions that enhance operational efficiency and support sustainable agricultural practices. The company's commitment to quality and innovation ensures that their products meet the highest standards in the industry, making them a trusted choice for businesses in the fertilizer sector.




