Sodium chlorate is a widely used chemical in various industrial applications, and the efficient handling of this material often requires specialized equipment. A sodium chlorate pneumatic conveyor is a critical piece of machinery designed to transport sodium chlorate powder or granules through a system using air pressure. This equipment plays a vital role in ensuring safe and effective material transfer, especially in environments where traditional bulk handling methods may pose challenges.

Design Principles of Pneumatic Conveying Systems
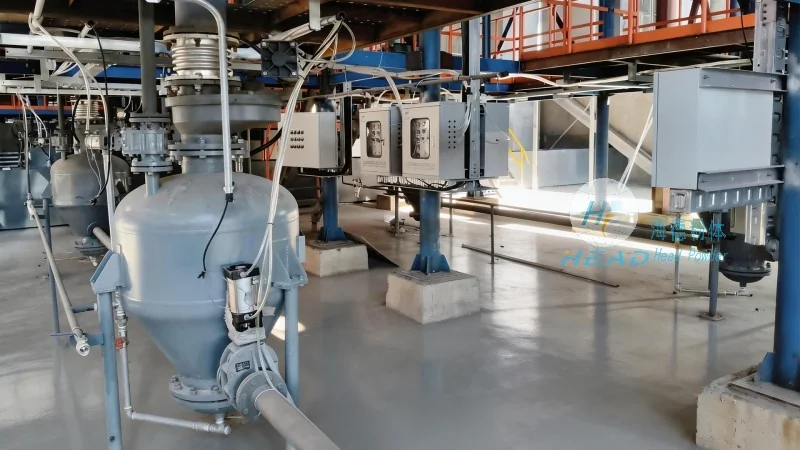
The design of a sodium chlorate pneumatic conveyor is based on fundamental principles of fluid dynamics and material handling. At its core, the system operates by creating a flow of air or other gas through a pipeline, which then propels the sodium chlorate particles. The key components include a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the material at the destination. The design must consider factors such as the material's properties—like its density, flowability, and potential for dust generation—as well as the required distance and throughput. Engineers at Shandong HeadPowder Engineering Co., Ltd. specialize in tailoring these systems to meet specific operational needs, ensuring optimal performance and safety.
Key Components and Their Functions
Each component of a sodium chlorate pneumatic conveyor contributes to the overall efficiency and reliability of the system. The hopper serves as the storage vessel, providing a consistent supply of material to the feeder. The feeder, often a rotary valve or a screw feeder, regulates the amount of sodium chlorate released into the conveying line, preventing overloading and maintaining a steady flow. The conveying line, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the chemical properties of sodium chlorate and the abrasive nature of the material. The air compressor or blower generates the necessary air pressure, which is then introduced into the line to move the particles. The receiver, usually a hopper or a storage bin, collects the material at the end of the conveying process. The entire system is often equipped with control valves and sensors to monitor pressure, flow, and material level, ensuring smooth operation and preventing blockages or other issues.
Advantages of Using Pneumatic Conveyors for Sodium Chlorate
Compared to traditional methods like belt conveyors or bucket elevators, pneumatic conveyors offer several advantages when handling sodium chlorate. One of the primary benefits is the ability to transport material in a closed system, which minimizes dust exposure and reduces the risk of contamination. This is particularly important for sodium chlorate, which can be hazardous if inhaled or come into contact with skin. Additionally, pneumatic conveyors can handle materials with varying flow properties, including those that are cohesive or have a tendency to agglomerate. The flexibility of the system allows for vertical, horizontal, or combined vertical and horizontal conveying, making it suitable for complex layouts. Another advantage is the reduced need for maintenance, as there are fewer moving parts compared to mechanical conveyors. The system is also energy-efficient, as the air pressure can be adjusted to match the material's requirements, optimizing energy consumption.

Applications and Industries
Sodium chlorate pneumatic conveyors are used in a variety of industries where sodium chlorate is a key ingredient. These include the pulp and paper industry, where it is used as a bleaching agent; the textile industry, for dyeing and finishing processes; and the chemical industry, for the production of other chemicals. In the agricultural sector, sodium chlorate is sometimes used as a herbicide, and pneumatic conveyors are employed to transport it from storage to application equipment. The versatility of the system makes it suitable for both large-scale industrial operations and smaller-scale applications, such as in research laboratories or small-scale chemical plants.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pneumatic conveying systems and related equipment. With a focus on innovation and customer satisfaction, the company has built a reputation for providing high-quality, reliable solutions for material handling challenges. HeadPowder specializes in customizing pneumatic conveyor systems to meet the specific needs of clients, ensuring that each system is optimized for the material being handled and the operational environment. The company's headquarters is located in Shandong, China, where it has a team of experienced engineers and technicians dedicated to research, development, and production. HeadPowder's commitment to quality and safety is evident in its adherence to industry standards and its use of advanced manufacturing techniques. By partnering with HeadPowder, clients can benefit from expert guidance and tailored solutions that enhance their operational efficiency and safety.




