HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced dust-free and airtight material conveying systems. These systems are engineered to ensure the safe and efficient transport of bulk materials while maintaining stringent environmental and operational standards. The following content provides a detailed overview of the operation process and working principle of such systems, highlighting the key components and mechanisms that contribute to their effectiveness.
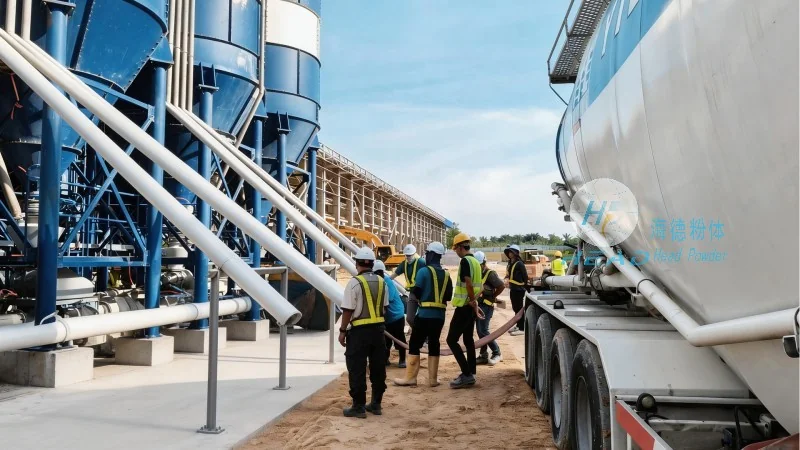
Company Profile and Background
HeadPowder Engineering Co., Ltd. is a professional enterprise based in Shandong, China. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and hygienic material handling solutions. The company's headquarters and main operational facilities are located in Shandong, where it leverages advanced technology and experienced engineering teams to develop customized conveying systems tailored to diverse industrial needs.
Overview of Dust-Free and Airtight Material Conveying Systems
The dust-free and airtight material conveying systems developed by HeadPowder are specifically designed to address the challenges of transporting bulk materials in environments where contamination control is critical. These systems utilize a combination of sealed components, positive pressure or vacuum mechanisms, and advanced sealing technologies to prevent the release of dust or other particulate matter into the surrounding air. The primary goal is to maintain a clean and safe working environment while ensuring the integrity and quality of the conveyed materials.

Operation Process of the Conveying System
The operation process of a typical dust-free and airtight material conveying system involves several sequential steps, each designed to ensure smooth and efficient material transport. The process begins with the loading of the bulk material into the initial hopper or storage container. From there, the material is fed into the conveying line through a sealed inlet, which is equipped with a suitable feeding mechanism such as a rotary valve or a screw feeder. The material then travels through the sealed pipeline, which is constructed from materials like stainless steel or food-grade plastic to prevent corrosion and contamination. As the material moves through the pipeline, it is propelled by positive pressure or vacuum, depending on the system design. The sealed outlets at the receiving end allow the material to be discharged into the target container or processing equipment without exposing it to the external environment. Throughout the entire process, the system maintains a controlled internal pressure to prevent external air from entering and to contain any potential dust emissions.

Working Principle of the System
The working principle of the dust-free and airtight material conveying system is based on the principles of fluid dynamics and sealed material transport. The system operates by creating a continuous flow of material within a sealed environment, ensuring that no air or contaminants can enter or escape from the pipeline. The key components include the feeding device, the conveying pipeline, the driving mechanism (such as a blower or vacuum pump), and the sealing elements (like gaskets and flanges). The feeding device controls the rate at which material is introduced into the system, while the driving mechanism provides the necessary force to move the material through the pipeline. The sealed pipeline is designed with tight connections and robust sealing mechanisms to maintain the integrity of the system. When the system is in operation, the internal pressure is maintained at a level that is slightly higher than the external ambient pressure (in positive pressure systems) or slightly lower (in vacuum systems), preventing the ingress of external air and the release of dust particles. This pressure differential is crucial for maintaining the dust-free and airtight characteristics of the system.

Key Features and Benefits
HeadPowder's dust-free and airtight material conveying systems offer several key features and benefits that make them ideal for various industrial applications. These include: 1) Strict contamination control, as the sealed design prevents dust and other particulates from entering or leaving the system; 2) Enhanced safety for operators, as the system eliminates the risk of exposure to hazardous materials; 3) Improved material quality, as the sealed environment prevents moisture absorption or contamination from external sources; 4) Energy efficiency, as the systems are designed to operate with minimal energy consumption; and 5) Customizability, allowing the company to tailor the system to specific customer requirements. The systems are suitable for a wide range of materials, including powders, granules, and bulk solids, and can be integrated into existing production lines or used as standalone solutions.
Conclusion
HeadPowder Engineering Co., Ltd. provides comprehensive dust-free and airtight material conveying solutions that combine advanced technology with rigorous engineering standards. The operation process and working principle of these systems ensure reliable and efficient material transport while maintaining stringent environmental and operational requirements. By leveraging the expertise and resources of HeadPowder, industries can achieve improved productivity, enhanced safety, and better material quality in their material handling operations.




