Ammonium nitrate (AN) is a widely used industrial chemical, often in its powdered form with moisture content. The efficient and safe transportation of such powders is crucial for industrial applications. This article provides an in-depth look at the operation process and working principle of specialized equipment designed for conveying ammonium nitrate powder with moisture content, highlighting the technical aspects and practical applications.

Overview of Ammonium Nitrate Powder with Moisture Conveying Equipment
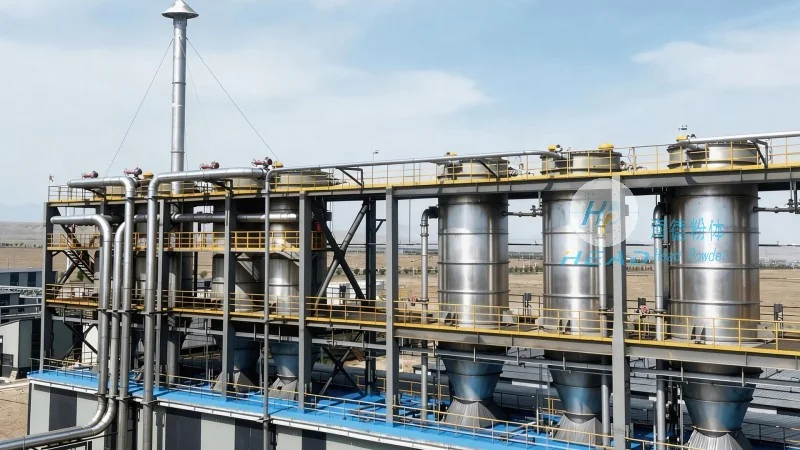
The equipment developed by Shandong HeadPowder Engineering Co., Ltd. is engineered to handle ammonium nitrate powders that contain a certain level of moisture. This is particularly important in processes where the material's moisture content affects its flowability and handling characteristics. The system is designed to ensure reliable and safe material transport, meeting the demands of various industrial sectors such as fertilizer production, chemical processing, and material handling.
Key Components and Their Functions
The conveying equipment typically consists of several key components that work in tandem to achieve efficient powder transport. These include a hopper for material storage, a conveyor system (often a screw or pneumatic conveyor), and a control unit for regulating the process. The hopper is designed to accommodate the bulk of the ammonium nitrate powder, ensuring a steady feed to the conveyor. The conveyor system, whether mechanical or pneumatic, is selected based on the specific properties of the powder, such as its moisture content and particle size. The control unit monitors parameters like flow rate, pressure, and temperature to maintain optimal operation and prevent issues like clogging or material degradation.

Operation Process of the Conveying Equipment
The operation process begins with the loading of ammonium nitrate powder with moisture into the hopper. The material is then fed into the conveyor system through a feeder mechanism, which ensures a consistent flow rate. The conveyor transports the powder through a pipeline or a series of connected components to the desired destination, such as a storage silo or processing unit. Throughout the process, the system continuously monitors the moisture content and flow characteristics of the powder to adjust the operation as needed. For example, if the moisture level changes, the system may adjust the conveyor speed or pressure to maintain stable transport. The entire process is automated, with minimal human intervention required, enhancing efficiency and safety.

Working Principle of the Equipment
The working principle of the conveying equipment is based on the physical properties of the ammonium nitrate powder with moisture. The equipment utilizes a combination of mechanical force and, in some cases, pneumatic pressure to move the material. The screw conveyor, for instance, rotates to push the powder forward, while the pneumatic system uses compressed air to create a flow of the material through the pipeline. The moisture content of the powder affects its bulk density and flowability, which in turn influences the required power and pressure for effective transport. The system is designed to handle these variations, ensuring that the powder is conveyed without excessive pressure or friction that could lead to degradation or safety hazards. The control unit plays a critical role in maintaining the balance between these factors, optimizing the operation for maximum efficiency and minimal energy consumption.
Benefits and Applications
The use of specialized conveying equipment for ammonium nitrate powder with moisture offers several benefits. Firstly, it ensures the safe and efficient transport of the material, reducing the risk of spills or accidents. Secondly, it maintains the quality of the powder by preventing segregation or degradation during transport. Thirdly, the automated system enhances operational efficiency, reducing labor costs and increasing production throughput. The equipment is widely used in the fertilizer industry, where ammonium nitrate is a key component of nitrogen-based fertilizers. It is also applied in chemical processing plants and other industrial settings where the handling of moisture-containing powders is required.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced conveying equipment for ammonium nitrate powder with moisture, combining technical expertise and practical design to meet the needs of various industrial applications. The operation process and working principle of this equipment ensure reliable and safe transport of the material, contributing to the efficiency and safety of industrial operations. By understanding the components, operation, and benefits of this equipment, users can make informed decisions about its application in their processes, leading to improved performance and reduced operational risks.




