HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of pneumatic conveying equipment for powder handling applications. This article explores the fundamental principles behind powder bin pneumatic conveying systems and highlights the key characteristics of their operational scenarios.

Understanding the Principle of Powder Bin Pneumatic Conveying
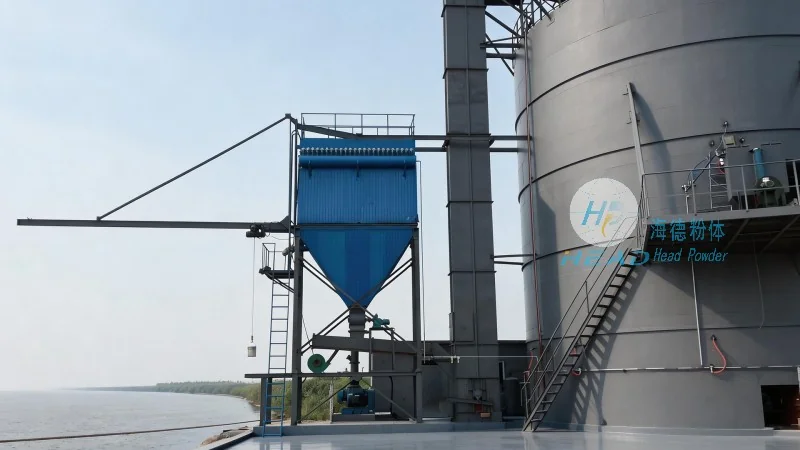
The core of a powder bin pneumatic conveying system lies in the use of compressed air to transport bulk powders from a storage bin to a processing or discharge point. The system typically consists of a powder bin, a conveying line, a control valve, and a receiver. When the system is activated, compressed air is introduced into the conveying line, creating a low-pressure zone that draws the powder from the bin into the line. The powder is then carried through the line by the air flow, reaching the destination where it is discharged under controlled conditions. This method eliminates the need for mechanical components like belts or screws, reducing maintenance and increasing safety in handling fine powders.

Key Working Scene Characteristics
The operational characteristics of powder bin pneumatic conveying systems are tailored to meet the demands of various industrial applications. These systems are particularly effective in environments where dust control and hygiene are critical, such as in pharmaceutical, food processing, and chemical industries. The enclosed design of the conveying line prevents dust from escaping into the workplace, ensuring compliance with environmental regulations and maintaining a clean working environment. Additionally, the flexibility of the system allows for multiple discharge points from a single bin, enabling efficient distribution of powders to different processing units or storage locations.
Advantages in Different Industrial Settings
In pharmaceutical manufacturing, the precision and cleanliness of pneumatic conveying systems are essential for maintaining product quality and regulatory standards. The system's ability to handle sensitive powders without contamination makes it ideal for applications like drug formulation and packaging. Similarly, in the food industry, the hygienic design and ability to handle food-grade powders without cross-contamination are crucial. The system's compact and modular design also allows for easy integration into existing production lines, minimizing downtime during installation and operation.
Efficiency and Reliability in Bulk Material Handling
Bulk material handling in industries like chemical and mining often requires high-capacity and reliable conveying solutions. The powder bin pneumatic conveying system offers high throughput rates, capable of transporting large volumes of powders over long distances with minimal energy consumption. The system's self-cleaning features, such as the use of reverse air flow to clear blockages, enhance its reliability and reduce downtime. Furthermore, the system's ability to handle a wide range of powder properties, including different particle sizes and moisture contents, makes it versatile for various applications. This adaptability ensures that the system can be optimized for specific material characteristics, improving overall operational efficiency.

Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides advanced powder bin pneumatic conveying solutions that combine efficiency, reliability, and compliance with industry standards. By leveraging the principles of pneumatic transport, these systems offer a cost-effective and safe method for handling bulk powders in diverse industrial settings. The company's commitment to quality and innovation ensures that their equipment meets the evolving needs of modern manufacturing processes, supporting industries in achieving higher productivity and operational excellence.




