HeadPowder, a leading enterprise in the field of bulk powder handling technology, specializes in providing advanced solutions for dust-free bag opening and pneumatic conveying systems. This article delves into the fundamental principles behind these technologies and explores the diverse operational environments where they are applied, highlighting the efficiency and safety advantages they offer in industrial settings.

Understanding the Core Principles of Dust-Free Bag Opening and Pneumatic Conveying
The process of dust-free bag opening and pneumatic conveying involves several key components and mechanisms designed to handle bulk powders without generating airborne dust. At the heart of this system is the bag opening mechanism, which safely and efficiently removes the contents of a sealed bag while maintaining a controlled environment. This is typically achieved through a combination of mechanical and pneumatic actions that gently break the bag's seal and release the powder into a receiving hopper or conveyor system. The pneumatic conveying section then uses air pressure to transport the powder from the opening station to the final destination, such as a storage silo, processing unit, or packaging line. The entire process is engineered to minimize dust generation, ensuring compliance with environmental regulations and maintaining a clean working environment.

Key Components and Their Functions in the System
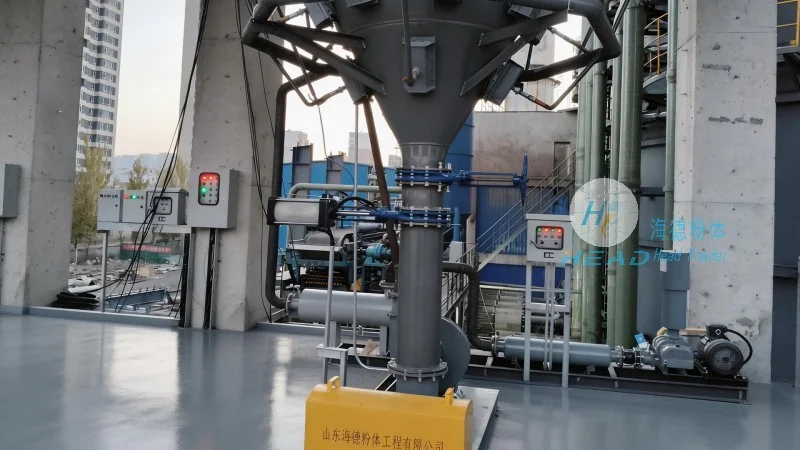
Several critical components work in tandem to ensure the smooth operation of a dust-free bag opening and pneumatic conveying system. The bag opening unit, often equipped with a vacuum or air-assisted mechanism, is responsible for accessing the bag's contents without compromising the integrity of the surrounding area. The conveying pipeline, which may include flexible hoses or rigid ducts, is designed to handle the powder's flow characteristics, such as particle size, density, and moisture content. Air compressors or blowers provide the necessary pressure to move the powder through the system, while filters and cyclones are used to separate any remaining particles from the air, preventing dust from escaping into the environment. Additionally, control systems, including sensors and valves, monitor the flow rate and pressure, ensuring optimal performance and preventing system overloads.

Application Scenarios and Operational Environments
The versatility of dust-free bag opening and pneumatic conveying makes it suitable for a wide range of industrial applications. In pharmaceutical manufacturing, for example, these systems are used to handle sensitive powders that require strict contamination control, ensuring product purity and safety. In food processing facilities, the technology is employed to transport ingredients like flour, sugar, and spices while maintaining hygiene standards and preventing cross-contamination. The chemical industry also benefits from this technology, as it allows for the safe handling of hazardous powders, reducing the risk of dust explosions and exposure to harmful substances. Furthermore, in the agricultural sector, dust-free systems are used to convey fertilizers and other bulk materials, improving efficiency and reducing environmental impact. Each of these applications leverages the system's ability to handle powders in a controlled, dust-free manner, enhancing operational safety and productivity.
Benefits and Advantages of Implementing Dust-Free Systems
Adopting dust-free bag opening and pneumatic conveying systems offers numerous benefits for industrial operations. One of the primary advantages is the significant reduction in airborne dust, which not only improves workplace safety by minimizing respiratory hazards but also enhances product quality by preventing contamination. The systems also contribute to better environmental compliance, as they help meet regulations related to dust emissions and air quality. From an operational perspective, these systems can increase efficiency by automating the bag opening and conveying process, reducing manual labor and minimizing downtime. The controlled environment also helps maintain consistent product quality, as the powder is handled gently and without exposure to external contaminants. Additionally, the modular design of many systems allows for easy integration into existing production lines, making it a cost-effective solution for businesses looking to upgrade their bulk handling capabilities.
Conclusion and Future Trends
As industries continue to prioritize safety, efficiency, and environmental responsibility, dust-free bag opening and pneumatic conveying systems remain a critical component of modern bulk powder handling. The technology's ability to handle a wide range of powders in a controlled manner makes it an essential solution for industries ranging from pharmaceuticals to food processing. With ongoing advancements in materials and control systems, these technologies are likely to become even more efficient and versatile in the future. For businesses seeking to enhance their operational performance while maintaining high standards of safety and quality, investing in a dust-free bag opening and pneumatic conveying system is a strategic decision that can yield long-term benefits.




