Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized material handling solutions for rare earth powders. Based in Shandong, China, our company, commonly known as HeadPowder, focuses on delivering efficient and reliable systems for the transport and processing of rare earth materials. This article explores the fundamental principles behind rare earth powder material transport and highlights the key characteristics of various working scenarios where these systems are applied.
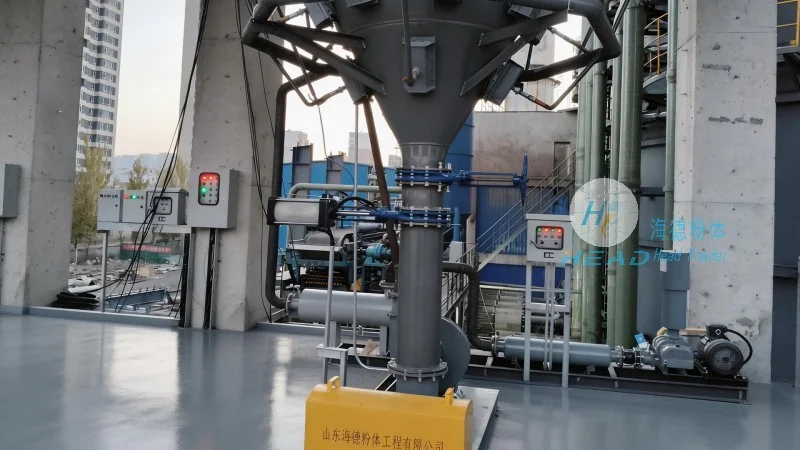
Principles of Rare Earth Powder Material Transport
The transport of rare earth powders requires careful consideration of several critical factors to ensure efficiency, safety, and product integrity. At the core of these systems are mechanisms designed to handle the unique properties of rare earth powders, such as their fine particle size, hygroscopic nature, and potential for static charge accumulation. The primary principles include:
1. Controlled Flow and Prevention of Agglomeration: Rare earth powders are prone to clumping or agglomeration, which can disrupt flow and affect downstream processing. Advanced transport systems employ techniques like vibration, air-assisted flow, or specialized conveyor designs to maintain a consistent, free-flowing material stream. This ensures that the powder moves smoothly through pipelines, hoppers, and processing equipment without clogging or uneven distribution.
2. Electrostatic Discharge Management: Due to their fine particle size, rare earth powders can generate static electricity during handling. This can lead to material buildup on surfaces or even spark hazards. Effective transport systems incorporate grounding mechanisms, anti-static additives, or conductive materials to mitigate static discharge risks. Proper grounding and regular maintenance of equipment are essential to prevent static-related issues and maintain operational safety.

3. Temperature and Environmental Control: Many rare earth compounds are sensitive to temperature fluctuations and moisture. The transport process must maintain stable environmental conditions to preserve the material's quality and prevent degradation. Systems often include temperature-controlled enclosures, moisture barriers, and sealed pipelines to protect the powder from external influences. This is particularly important for materials used in high-tech applications where purity and consistency are paramount.
Key Characteristics of Working Scenarios in Rare Earth Powder Handling
The application of rare earth powder transport systems varies widely depending on the specific industrial context. Understanding these working scenarios helps in selecting the most appropriate equipment and ensuring optimal performance. Here are some common scenarios and their defining characteristics:
1. Industrial Production Lines: In large-scale manufacturing facilities, rare earth powders are often integrated into automated production lines for the production of magnets, catalysts, and other high-value products. The transport systems in these scenarios must support high throughput, consistent material flow, and seamless integration with other processing equipment. For example, in a magnet manufacturing plant, rare earth powders may be transported from storage silos to mixing and pressing stations via pneumatic conveyors or screw conveyors. The systems need to handle large volumes of material while maintaining precise control over particle size distribution and moisture content.
2. Research and Development Laboratories: In R&D settings, the handling of rare earth powders is typically on a smaller scale but requires high precision and flexibility. Laboratory-scale transport systems may include manual or semi-automated conveyors, such as small pneumatic lines or precision screw feeders. These systems are designed to handle small batches of material and allow for easy adjustment of flow rates and particle size. The focus here is on maintaining the purity of the powder and enabling accurate experimentation. The systems must also be easy to clean and maintain to prevent cross-contamination between different samples.

3. Storage and Distribution Centers: Rare earth powders are often stored in bulk quantities before distribution to various customers or processing facilities. The transport systems in storage centers are focused on efficient loading and unloading of bulk containers, such as silos, hoppers, or bulk bags. These systems may include bulk material handling equipment like bucket elevators, belt conveyors, or pneumatic transfer systems. The key characteristics here are reliability, durability, and the ability to handle large volumes of material over extended periods. Proper storage also involves controlling environmental factors like temperature and humidity to prevent material degradation.
4. Environmental and Safety Compliance: Given the hazardous nature of some rare earth compounds and the need to comply with environmental regulations, transport systems must adhere to strict safety and environmental standards. This includes features like dust suppression systems, enclosed conveyor designs to prevent dust emissions, and proper waste management protocols. The systems are designed to minimize the risk of exposure to workers and to protect the environment from contamination. Compliance with local regulations and industry standards is a critical aspect of successful rare earth powder handling operations.
Conclusion: The Importance of Specialized Material Handling Solutions
Efficient and reliable transport of rare earth powders is essential for the success of various industrial applications. The principles and working scenarios discussed above highlight the complexity and importance of specialized material handling systems. At Shandong HeadPowder Engineering Co., Ltd., we understand the unique challenges associated with rare earth powder transport and offer tailored solutions to meet the specific needs of our clients. By focusing on controlled flow, electrostatic management, and environmental control, our systems ensure the integrity of the material while maintaining operational safety and efficiency. Whether for large-scale production, laboratory research, or bulk storage, our expertise in rare earth powder handling enables businesses to achieve their goals with confidence. Contact us today to learn more about how our solutions can enhance your material handling processes.




