Dense phase powder transport systems represent a sophisticated method for handling and conveying bulk powders. These systems are designed to operate under high pressure, enabling the efficient movement of materials like cement, coal, and other fine particulates. The core principle involves creating a slurry-like mixture by injecting air or gas into the powder stream, which reduces friction and allows for smooth, continuous transport. This approach is particularly advantageous in industrial settings where traditional pneumatic or mechanical conveying methods may face challenges such as blockages or excessive energy consumption.

Working Principle of Dense Phase Conveying
The fundamental mechanism of dense phase powder transport relies on the creation of a dense, non-eroding flow. By pressurizing the system and introducing a controlled amount of gas into the powder, the material is forced to move in a plug flow rather than a dilute, turbulent state. This results in reduced particle attrition and improved system efficiency. The process typically involves a hopper or feeder that feeds the powder into a pipeline, where the gas is introduced to maintain the dense phase. The pressure differential between the inlet and outlet drives the material forward, ensuring consistent flow rates and minimal pressure drop over long distances.
Key Components and System Design
HeadPowder Engineering Co., Ltd. specializes in the design and implementation of dense phase powder transport systems. The core components include a feeding mechanism, a pressure vessel or pump, a gas injection system, and a pipeline network. The feeding system ensures a steady supply of powder, while the pressure vessel maintains the necessary pressure to initiate the dense phase flow. The gas injection system is critical, as it controls the air-to-powder ratio to achieve optimal conveying conditions. The pipeline design must consider factors such as material compatibility, pressure ratings, and the need for minimal bends or obstructions to maintain the dense flow.

Application Scenarios and Operational Advantages
Dense phase powder transport systems are widely used in various industrial applications. In the cement industry, these systems facilitate the efficient transport of raw materials and finished products, reducing downtime and improving production throughput. In coal handling facilities, they enable safe and reliable movement of coal from storage to processing units, minimizing dust emissions and operational risks. Additionally, in chemical and pharmaceutical sectors, dense phase conveying is employed to transport sensitive powders, ensuring product integrity and compliance with regulatory standards. The operational advantages include lower energy consumption compared to pneumatic systems, reduced maintenance requirements due to the absence of moving parts in the conveying line, and improved material handling safety by minimizing dust exposure.
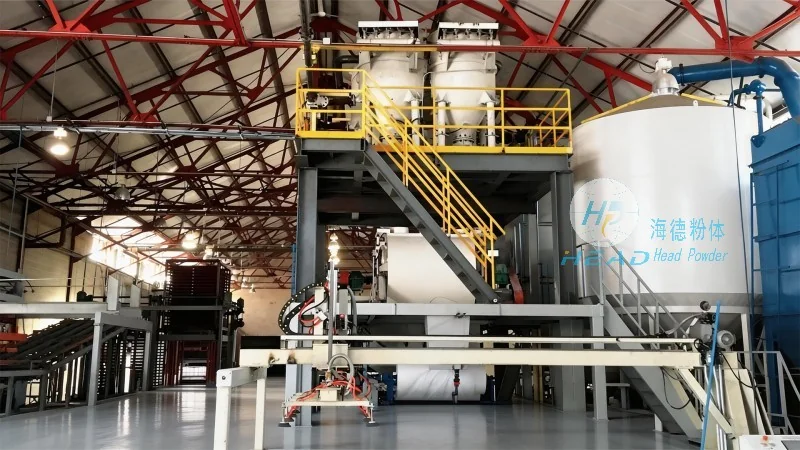
Case Study: Industrial Implementation in Shandong, China
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented dense phase powder transport systems for a major cement manufacturer in Shandong, China. The project involved designing a system capable of transporting 100 tons of cement per hour over a distance of 500 meters. The system was tailored to handle the specific characteristics of the cement, including its fine particle size and cohesive properties. The implementation resulted in a 20% reduction in energy consumption compared to traditional conveying methods and a significant decrease in operational downtime due to reduced blockages. The success of this project highlights the effectiveness of dense phase technology in addressing the unique challenges of bulk powder handling in industrial settings.
Conclusion and Future Developments
Dense phase powder transport systems offer a robust and efficient solution for bulk powder handling, with applications spanning multiple industries. As technology advances, there is ongoing research into improving system efficiency, such as optimizing gas injection patterns and enhancing material compatibility. HeadPowder Engineering Co., Ltd. continues to innovate in this field, providing tailored solutions that meet the specific needs of clients. The integration of advanced control systems and predictive maintenance further enhances the reliability and longevity of these systems, ensuring they remain a preferred choice for industrial powder transport applications.




