HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. Among their product lineup, the powder bin pneumatic conveying system stands out as a critical solution for efficient material transport in various industrial applications. This article delves into the fundamental principles of this technology and highlights its key working characteristics and typical application scenarios.

Understanding the Core Principle of Powder Bin Pneumatic Conveying
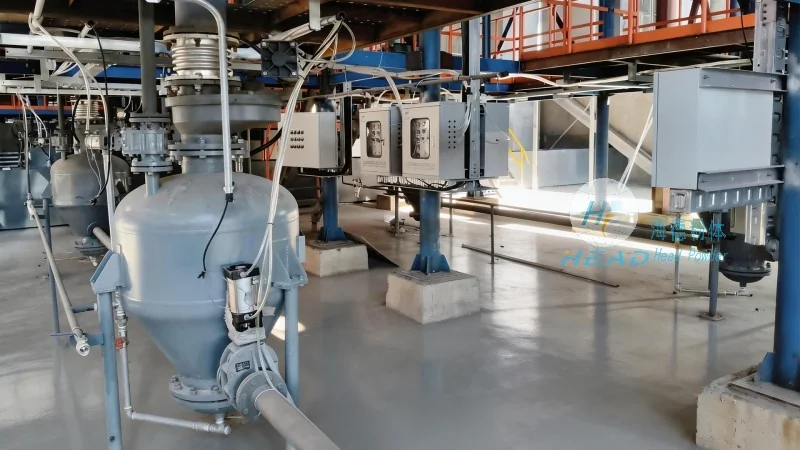
The powder bin pneumatic conveying system operates on the principle of air movement to transport bulk powders from a storage bin to a processing or discharge point. At its heart, the system utilizes a combination of air pressure and vacuum to create a flow of material. The process typically begins with the material being drawn from the powder bin by a vacuum or pressure differential. The air, either under pressure or suction, carries the powder particles through a pipeline network, ensuring smooth and continuous transport. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational reliability.

Key Working Characteristics of the System
Several distinct characteristics define the performance of a powder bin pneumatic conveying system. First, the system offers high flexibility in terms of layout and routing. The pipelines can be configured in various configurations, including vertical, horizontal, or a combination of both, to suit the spatial constraints of a facility. This adaptability allows for efficient material transfer even in complex plant layouts. Second, the system provides excellent control over material flow rates. By adjusting the air pressure or vacuum levels, operators can precisely regulate the speed at which powders are conveyed, ensuring consistent processing conditions. Third, the technology minimizes material degradation and contamination. The enclosed pipeline system prevents exposure to external elements, reducing the risk of dust accumulation or cross-contamination. Additionally, the system is designed to handle a wide range of powder types, from fine powders to bulkier granules, with minimal loss or degradation.
Typical Application Scenarios
The powder bin pneumatic conveying system is widely used across multiple industries due to its versatility and efficiency. In the pharmaceutical industry, it is employed to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements. The enclosed system ensures that these materials remain uncontaminated and meet regulatory standards. In the food and beverage sector, the system is used for handling powders such as flour, sugar, and protein powders, maintaining hygiene and preventing cross-contamination. The chemical industry also relies on this technology for transporting various powders, including catalysts and reagents, where precise control and minimal contamination are essential. Furthermore, in the cement and construction materials industry, the system efficiently moves raw materials like limestone and clinker, improving production throughput and reducing labor costs.
Conclusion
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, continues to innovate in the field of powder handling technology. The powder bin pneumatic conveying system exemplifies the company's commitment to providing reliable, efficient, and cost-effective solutions for industrial material transport. By understanding the core principles and working characteristics of this system, industries can optimize their operations and enhance productivity. As a trusted manufacturer, HeadPowder remains dedicated to meeting the diverse needs of its clients, ensuring that their pneumatic conveying systems deliver superior performance and longevity.




