Bottom-hopper powder pneumatic conveying represents a sophisticated approach to material handling, particularly for the transport of dry powders from storage hoppers to processing equipment. This technology relies on the principles of air flow to create a pressure differential that entrains and transports powder particles through a pipeline system. The bottom-hopper design is a key feature, as it draws material from the lower portion of the storage vessel, which is crucial for preventing issues like bridging or caking that can occur in top-discharge configurations. This design enhances the system's reliability and efficiency, especially for cohesive or fine powders that are prone to flow problems.

Core Principle of Bottom-Hopper Pneumatic Conveying
The fundamental mechanism of bottom-hopper pneumatic conveying involves generating a flow of air that pulls or pushes the powder through the pipeline. In a suction system, the air is drawn from the discharge end, creating a negative pressure that pulls the powder from the hopper. In a pressure system, compressed air is introduced at the discharge end, pushing the powder forward. The bottom-hopper ensures that the powder is released from the lowest point of the vessel, allowing for a consistent and unobstructed flow. This approach minimizes the risk of material accumulation at the hopper outlet, which can lead to blockages and operational disruptions. The system's efficiency is further enhanced by the use of appropriate air velocities and pipeline diameters, which are tailored to the specific characteristics of the powder being conveyed.

Application Scenarios and Industrial Use Cases
Bottom-hopper pneumatic conveying is widely utilized across various industries due to its adaptability and effectiveness. In the chemical industry, it is commonly used to transport raw materials such as powders of pigments, catalysts, or reagents to reactors and mixers. The system's ability to handle abrasive or corrosive powders makes it ideal for these environments, where traditional mechanical conveyors may experience wear or contamination. For example, in a pigment manufacturing plant, the bottom-hopper system efficiently moves colored powders to the mixing tanks, ensuring consistent coloration and reducing the risk of material degradation. In the food and beverage sector, the technology is employed to transfer ingredients like flour, sugar, or spices to processing lines. The enclosed pipeline design maintains hygiene and prevents cross-contamination, which is critical for food safety regulations. Pharmaceutical applications also benefit from this technology, as it allows for the handling of sterile powders in GMP-compliant facilities. The system's ability to maintain a dust-free environment and prevent particle loss ensures product quality and regulatory compliance.

Advantages and Technical Benefits
Compared to alternative conveying methods, bottom-hopper pneumatic conveying offers several significant advantages. First, it provides a continuous and uniform flow of material, which improves production efficiency and reduces downtime. Unlike belt or screw conveyors that may require frequent stops for maintenance or material loading, pneumatic systems operate continuously, enhancing operational throughput. Second, the system is highly flexible, allowing for changes in the conveying route or destination without major structural modifications. This adaptability is particularly valuable in facilities where production lines are frequently reconfigured or expanded. Third, the bottom-hopper design reduces the risk of material degradation due to exposure to air or moisture. By keeping the powder within a sealed environment until it reaches the processing equipment, the system preserves the material's properties and quality. Additionally, the technology can handle a wide range of powder characteristics, including varying particle sizes, densities, and flowabilities. This versatility makes it suitable for diverse material types, from fine powders like talc to bulkier materials like limestone.
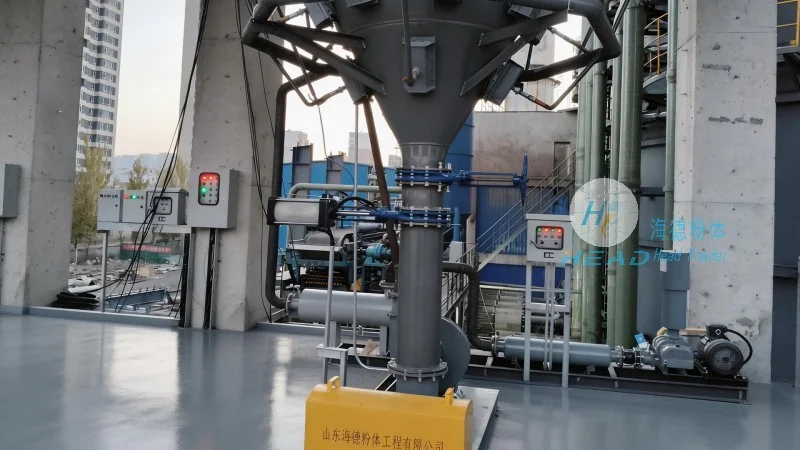
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a prominent player in the material handling industry, specializes in the development and implementation of bottom-hopper pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has built a reputation for delivering high-quality, customized solutions tailored to specific industrial needs. HeadPowder's expertise stems from decades of experience in designing and manufacturing material handling equipment, ensuring that each system is optimized for performance and longevity. The company's headquarters and manufacturing facilities are located in Shandong, China, where it leverages advanced manufacturing technologies and a skilled workforce to produce reliable and efficient products. By combining technical expertise with a customer-centric approach, HeadPowder helps clients enhance their operational efficiency, reduce material handling costs, and improve overall production output. The company's commitment to quality and service has made it a trusted partner for businesses seeking to optimize their powder transport processes.




