Working Principle and Features of Melamine Powder Material Handling System Equipment
Release time:2026-09-18 00:01:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Melamine powder is a widely used chemical compound in various industries, and efficient material handling is crucial for its processing and transportation. The melamine powder material handling system equipment, as provided by Shandong HeadPowder Engineering Co., Ltd., is designed to address the specific challenges associated with handling this fine powder. This article will explore the working principle and key features of such systems, highlighting how they enhance operational efficiency and safety in industrial applications.
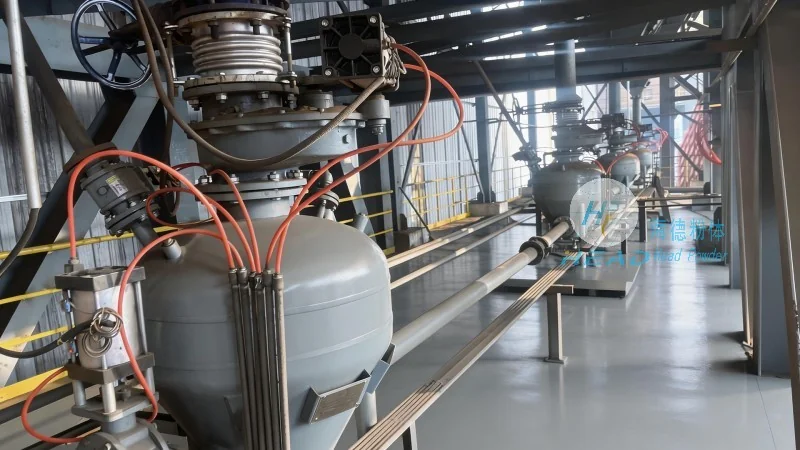


Working Principle of the Melamine Powder Material Handling System
The melamine powder material handling system operates on a principle of controlled and continuous material flow, ensuring minimal dust generation and product contamination. The system typically consists of several components, including feeders, conveyors, and dust collection units, all integrated to work in harmony. The process begins with the melamine powder being fed into the system via a hopper or bulk bag unloader. A precision feeder then regulates the flow rate, ensuring a consistent and controlled discharge into the conveyor. The conveyor, often a pneumatic or mechanical type, transports the powder to the desired destination, such as storage silos or processing units. Throughout the process, dust suppression mechanisms, like cyclone separators and bag filters, are employed to capture and recycle fine particles, maintaining a clean and safe working environment. The system's control panel allows for real-time monitoring and adjustment of parameters, such as flow rate and pressure, to optimize performance and prevent system overload.
Key Features of the Melamine Powder Material Handling System
Shandong HeadPowder Engineering Co., Ltd. offers a range of features that distinguish their melamine powder material handling systems from conventional solutions. Firstly, the system is engineered for high efficiency, with minimal downtime and maximum throughput. The use of advanced materials and robust construction ensures durability and long service life, reducing maintenance costs over time. Secondly, the system incorporates advanced dust control technology, which is critical for maintaining air quality and compliance with environmental regulations. The integrated dust collection system effectively captures and recycles fine powder, minimizing emissions and ensuring a safe working environment for operators. Thirdly, the system is designed for flexibility, allowing for easy integration with existing industrial setups. This adaptability enables seamless incorporation into production lines, without the need for extensive modifications. Additionally, the system features user-friendly controls, with intuitive interfaces that allow operators to monitor and adjust settings with ease. This reduces the learning curve and enhances overall operational efficiency. Finally, the system is built with safety in mind, incorporating features like emergency stop buttons and overload protection to prevent accidents and ensure the well-being of personnel.




