For industrial applications that require the efficient and safe transport of catalyst powders, specialized material handling systems are essential. These systems are designed to address the unique challenges posed by catalyst powders, such as their fine particle size, potential reactivity, and the need for contamination control. The following content provides an overview of the working principle and key features of catalyst powder material handling systems, along with information about the manufacturer, Shandong HeadPowder Engineering Co., Ltd., based in China.
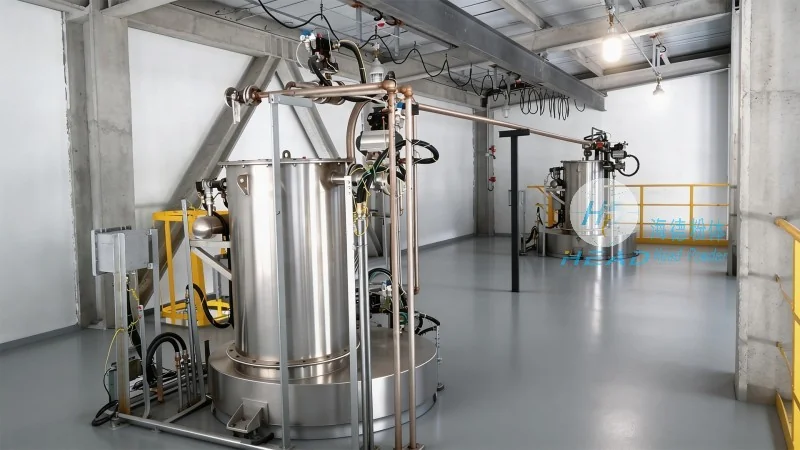

Understanding the Working Principle of Catalyst Powder Material Handling Systems
The core function of a catalyst powder material handling system is to move powders from one location to another within an industrial facility. The process typically involves several key components and steps. First, the catalyst powder is loaded into a storage hopper or silo. From there, it is transferred to a feeder, which controls the flow rate and ensures a consistent supply of material. The feeder may use mechanisms like rotary valves, vibratory feeders, or screw conveyors to regulate the discharge of powder. Next, the material is conveyed through a pipeline system, often using pneumatic or mechanical methods. Pneumatic conveying systems utilize compressed air to transport the powder in a sealed pipeline, while mechanical systems employ screw conveyors, belt conveyors, or bucket elevators. The system may also include filtration and dust collection equipment to maintain air quality and prevent particle loss. Finally, the powder is discharged at the destination point, such as a reactor or processing unit. The entire process is designed to be continuous, automated, and reliable, minimizing human intervention and ensuring precise control over the material flow.

Key Features of Catalyst Powder Material Handling Systems
Effective catalyst powder material handling systems are characterized by several important features that enhance performance and safety. One critical feature is the use of dust-tight and explosion-proof components, which are essential for handling potentially reactive or flammable powders. These systems often incorporate sealed hoppers, flexible hoses, and explosion-proof motors to prevent dust accumulation and minimize the risk of ignition. Another key feature is the ability to maintain a consistent flow rate, which is crucial for maintaining process stability in downstream equipment. This is achieved through advanced control systems that monitor pressure, flow, and temperature, and adjust the feeder or conveyor speed accordingly. Additionally, many systems include monitoring and alarm systems that detect deviations from normal operation, such as blockages or air leaks, and alert operators to take corrective action. The design also emphasizes material containment and cleanliness, with features like self-cleaning hoppers and sealed transfer points to prevent cross-contamination and product loss. Finally, the systems are typically constructed from materials that are resistant to corrosion and wear, ensuring long-term durability and low maintenance costs.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of specialized material handling equipment for the chemical and petrochemical industries. With its headquarters in Shandong, China, the company has extensive experience in designing and producing systems tailored to the unique needs of catalyst powder handling. HeadPowder's expertise lies in creating customized solutions that meet the specific requirements of each client, including considerations for powder properties, process conditions, and safety regulations. The company's commitment to quality and innovation has made it a trusted partner for businesses seeking reliable and efficient catalyst powder material handling systems. By leveraging advanced engineering and manufacturing capabilities, HeadPowder ensures that its products deliver optimal performance and longevity, helping clients improve operational efficiency and reduce downtime.




